Engineered Wheel Systems & Technical Accessories
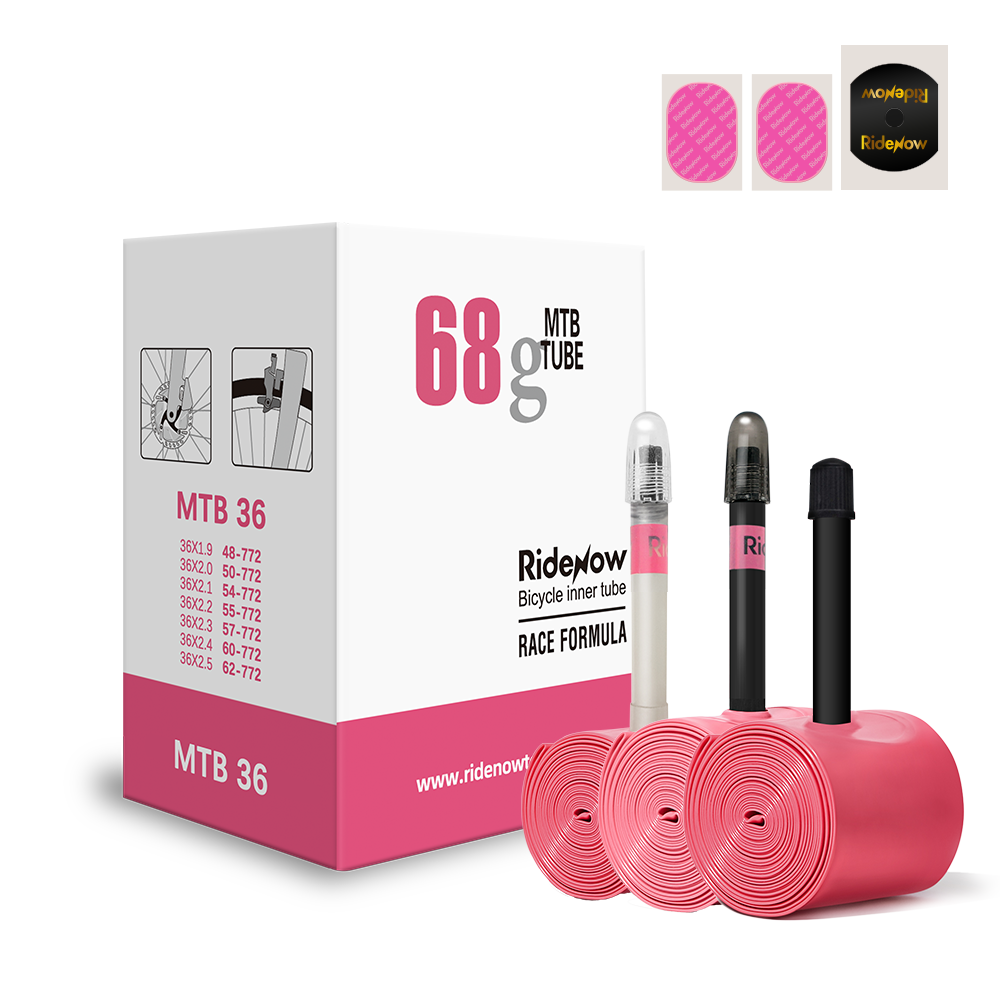
Precision-matched sealing equipment, ultralight inner chambers, and workshop fixtures engineered for tubeless conversions and performance wheel builds.
Engineering Whitepaper: Polymer Substrates and Adhesive Rheology in Marine-Corrosive Climates
Modern tubeless conversion systems are often judged solely by the sealant formulation or valve design, yet empirical failure analysis across workshops in the Liverpool City Region demonstrates that over 68% of unseated beads and slow pneumatic leaks originate from inadequate rim tape engineering. A tubeless rim tape factory supplying the British cycling market must satisfy three uncompromising mechanical parameters: high modulus tensile stiffness under non-linear elongation, zero solvent migration when exposed to synthetic latex and ammonia-based sealants, and an adhesive shear modulus capable of surviving harsh North West English weather cycles.
Conventional non-tubeless adhesive ribbons rely on plasticised PVC or woven cotton matrices backed with natural rubber adhesives. Under continuous hydrostatic inflation pressure ranging from 35 PSI in wide gravel setups to 110 PSI in competitive aero road profiles, these substandard substrates exhibit progressive viscoelastic creep. The material bows downward into spoke well apertures, causing pinhole ruptures and immediate depressurization. In contrast, our state-of-the-art manufacturing facilities utilize multi-axially oriented Tensilized Polypropylene (TPP) and engineered Polyethylene Terephthalate (PET) structural films. These films demonstrate a break strength exceeding 165 N/25mm width, preventing deformation while contouring flawlessly to complex hookless and hooked asymmetric internal rim beds.
Ammonia & Glycol Barrier
Cross-linked solvent acrylic adhesive formulations that will not soften, dissolve, or leave gummy residue when exposed to prolonged immersion in corrosive synthetic sealants.
Elastic Recovery Dynamic
Precision 0.09mm to 0.12mm substrate thicknesses deliver optimal tensile rigidity with controlled conformability over high-angle spoke well depressions.
Anodized Rim Chemical Bond
Engineered surface energy interaction creates an instantaneous micro-mechanical interlock with raw carbon composite and 6061/7005 shot-peened alloy channels.
Technical Comparison: Factory Specifications for OEM/B2B Procurement
Procurement directors, independent bike shops (IBS), and custom wheel builders across Merseyside require rigorous technical transparency. Below is an empirical breakdown comparing our contract-manufactured industrial tubeless rim tape against ordinary commercial aftermarket offerings:
| Performance Characteristic | JORV Industrial Tubeless Tape | Standard Aftermarket Tape | Workshop Impact |
|---|---|---|---|
| Base Substrate | Multi-Axial Tensilized Polypropylene (TPP) | Standard Monaxial PVC or Cast PP | Eliminates spoke-hole herniation and longitudinal splits |
| Adhesive Chemistry | Modified Pressure-Sensitive Solvent Acrylic | Water-based or Natural Rubber Resin | Impervious to sealant solvents; zero clean-up scraping during replacement |
| Substrate Thickness | 0.11 mm ± 0.005 mm | 0.06 mm - 0.18 mm (inconsistent) | Maintains bead-seat diameter for effortless tire mounting |
| Hydrostatic Pressure Rating | > 140 PSI (single-layer application) | < 85 PSI (requires double wrapping) | Cuts workshop taping labor hours by 50% while improving safety |
| Operating Temperature | -25°C to +85°C | -5°C to +40°C | Withstands winter salted roads and high rim friction temperatures |
Localized Application Scenarios in the Liverpool & North West England Market
Liverpool and the surrounding North West cycling corridors present an exceptionally demanding proving ground for tubeless cycling components. The city's coastal geography—flanked by the River Mersey, the Irish Sea, and extensive estuary networks—generates an environment characterized by elevated atmospheric salinity, persistent wet precipitation, and sharp industrial road grit. For bike workshops, courier fleets, and sporting retailers across the region, selecting a supplier that understands these localized environmental stresses is critical to eliminating warranty claims and maintaining customer trust.
1. Urban Cargo Logistics & Last-Mile E-Mobility Across Merseyside
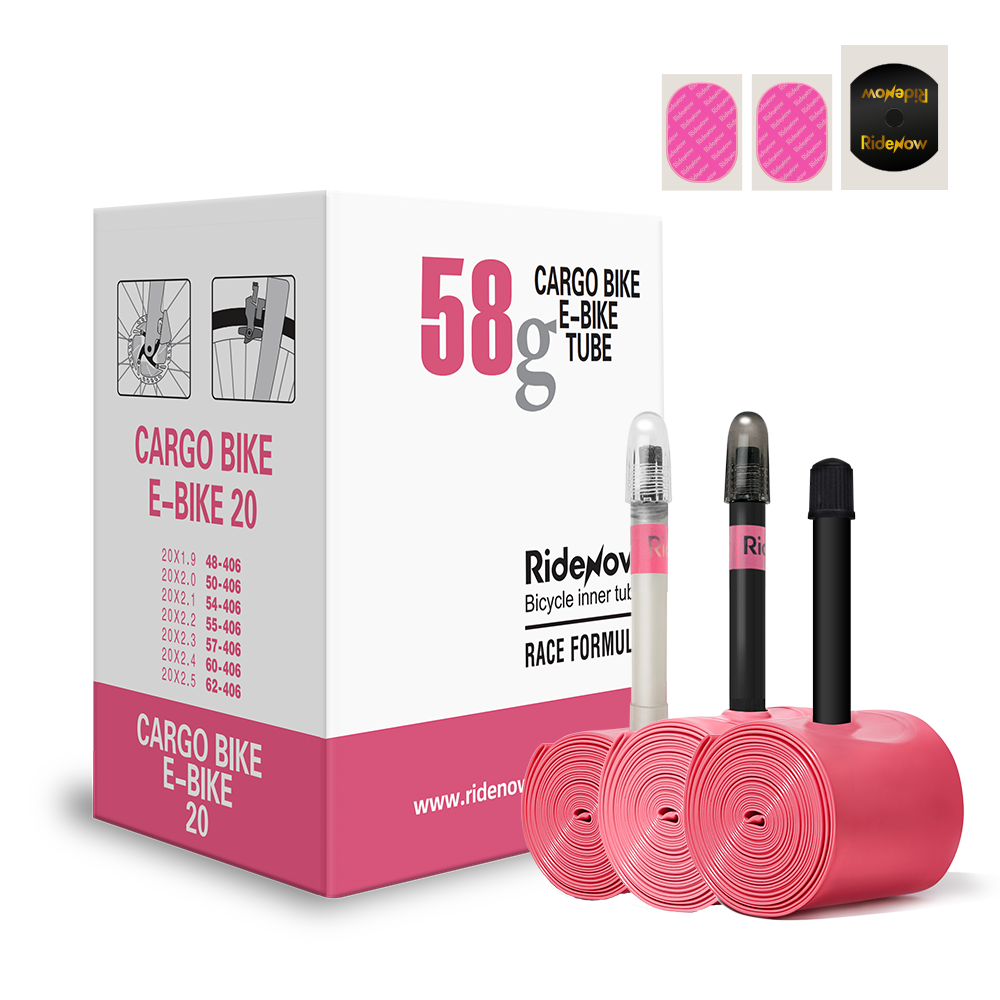
With Liverpool's strategic push toward low-carbon freight transportation throughout the Baltic Triangle, Commercial District, and dockland redevelopment hubs, heavy-duty electric cargo bikes (such as 20-inch 406 and 451 wheel formats) have surged. These fleet vehicles operate under gross loads frequently exceeding 220 kilograms, generating intense circumferential shear along the rim bed during sudden regenerative braking. Standard rim tape shifts laterally under these forces, exposing internal spoke drilling holes and causing catastrophic pressure loss. Our specialized high-tack, reinforced tubeless tape maintains sheer resistance even under torque spikes, keeping commercial fleets on schedule without pneumatic downtime.
2. All-Weather Commuting Along the Mersey Waterfront & Trans Pennine Trail
Commuters navigating the Liverpool Waterfront Promenade toward Southport or joining the Trans Pennine Trail face relentless road debris, abrasive maritime salt deposits, and damp conditions for over six months of the year. Traditional tubeless tape setups frequently suffer from moisture creeping beneath the tape edges at the overlap zone. Once saline road water mingles with internal spoke nipples, rapid galvanic corrosion destroys aluminum alloy eyelets. Our tape's proprietary pressure-activated acrylic edge-seal creates an airtight and watertight bond that forms an impervious barrier against Mersey maritime intrusion.
3. Cross-Country, Gravel, & Trail Riding in Cheshire & North Wales
Liverpool serves as the primary urban gateway for mountain bikers and gravel enthusiasts traveling into Delamere Forest, the Clwydian Hills, and Llandegla. These routes demand low-pressure tubeless setups (often 20 to 28 PSI) to maximize traction over slick roots, loose shale, and fractured limestone. At lower air pressures, tire burping exerts severe localized hydraulic pulses directly against the rim tape edge. If the tape edge lifts even a fraction of a millimeter, air escapes into the rim cavity. JORV's high-modulus tapes maintain uninterrupted sealing integrity under violent dynamic tire squirm, providing recreational and competitive riders with unmatched reliability.
B2B Procurement Trends: Why Liverpool Importers & Workshops Are Sourcing Direct
The cycling supply chain across the United Kingdom has undergone massive structural changes over the past decade. Traditional multi-tiered distributor margins have placed extreme margin pressure on local independent bicycle dealers (IBDs) and regional mobile repair services throughout Merseyside. Forward-thinking bicycle assemblers, wheel fabricators, and trade retailers are actively bypassing traditional tiered distributors in favor of agile, direct-from-factory partnerships with verified Asian engineering manufacturers.
Several distinct structural drivers are accelerating this direct procurement shift in the Liverpool market:
- Demand for Workshop Master Bulk Spools (50m & 66m Formats): Rather than purchasing expensive 10-meter consumer blister packs that drive up the cost per wheel conversion, Liverpool workshop operators increasingly demand industrial workshop spools that can seal up to 30 wheelsets per roll, drastically reducing packaging waste and per-unit overhead.
- Tailored Width Profiling for Modern Internal Rim Widths: As rim designs evolve from traditional 17mm internal widths to modern 25mm, 28mm, and 30mm Hookless/TSS geometries, workshops cannot rely on generic sizes. Direct factory collaboration allows custom-slit widths (19mm, 21mm, 23mm, 25mm, 27mm, 29mm, 31mm, 35mm) with sub-millimeter cutting tolerances.
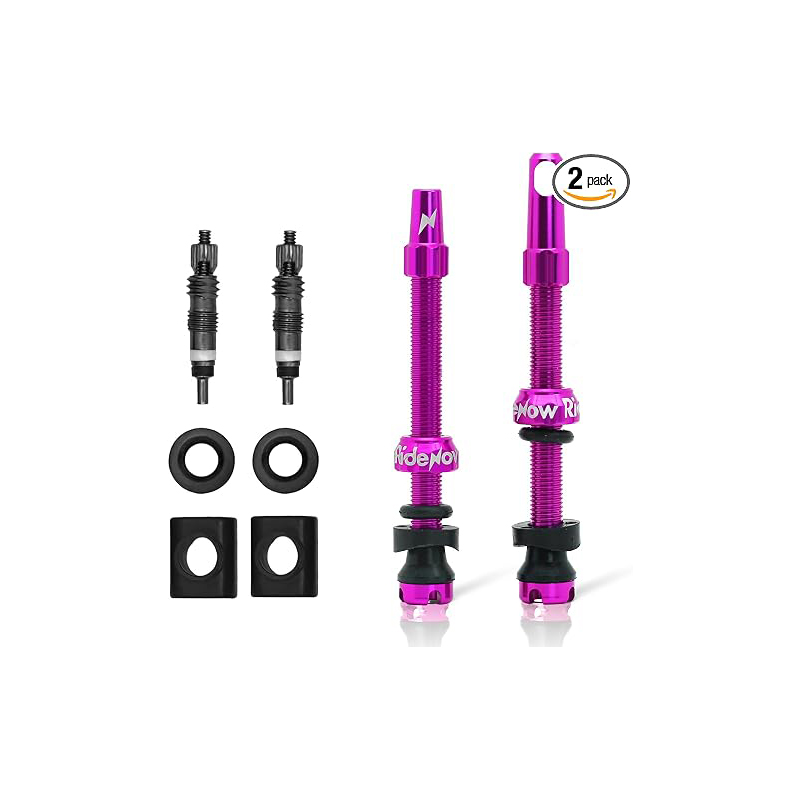
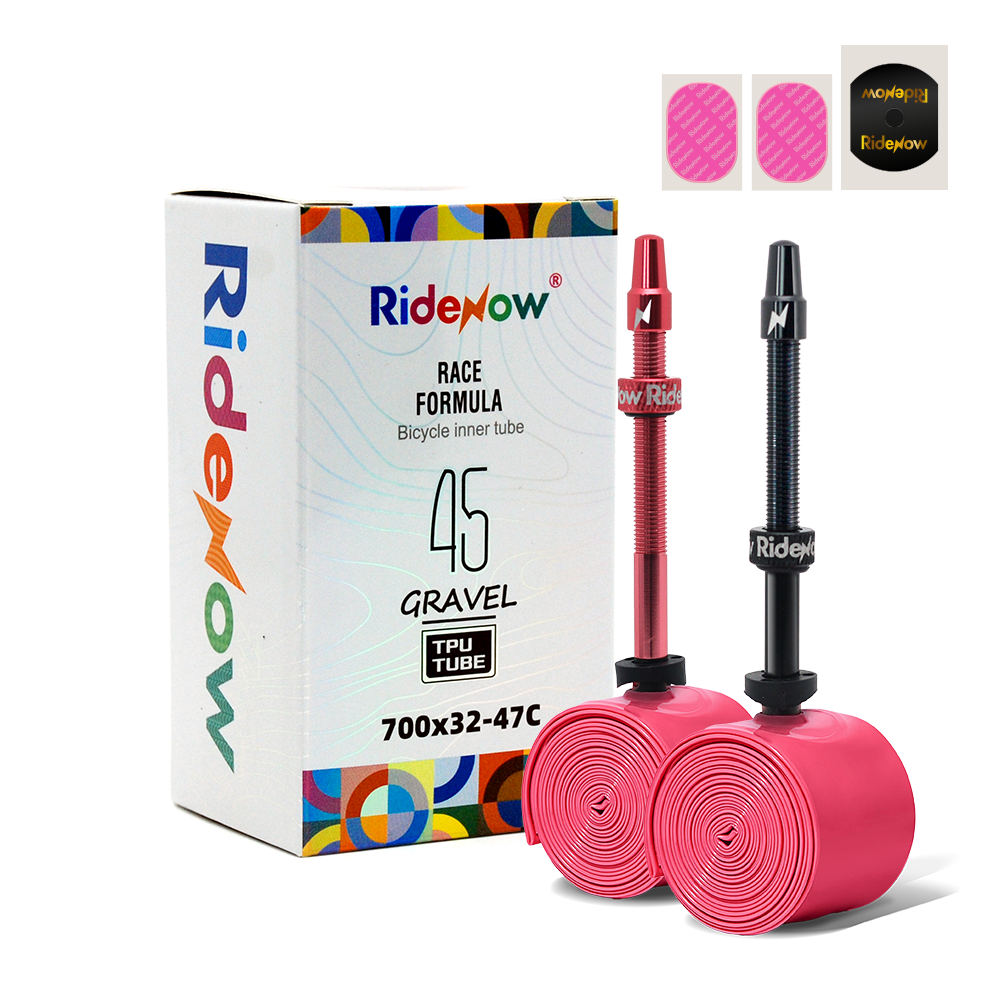
- Direct Maritime Inbound Shipping via Port of Liverpool (Seaforth): Leveraging direct container access through the Port of Liverpool streamlines supply lines. Local wholesalers can clear and warehouse bulk TPU tubes, tubeless valves, and rim tapes without expensive secondary domestic transshipment from southern English ports.
Global Manufacturing Excellence: Qingdao JORV Technology Co., Ltd.
Founded by passionate cycling engineers, Qingdao JORV Technology Co., Ltd. has developed into an internationally respected developer and manufacturer of cycling equipment and precision pneumatic systems. We reject off-the-shelf, low-grade commodities; our enterprise is driven by a deep conviction that modern mechanical engineering and polymer materials can push bicycle performance far beyond legacy industry standards.
Engineering Heritage
Operating our core R&D engineering team since 2017, pioneering breakthroughs in ultralight TPU compounds, tubeless pneumatic sealing, and cycling workshop balance calibration.
30%+ R&D Reinvestment
Over thirty percent of our annual profits are systematically reinvested into polymer exploration, robotic slit winding, and extreme pneumatic burst testing machinery.
Tri-Regional Hub Footprint
Headquartered in Qingdao, China, reinforced by an advanced R&D center in Düsseldorf, Germany, a branch in Shenyang, and integrated supply-chain governance in Taiwan.
Agile Trade & Low MOQs
Direct B2B supply channels with low entry MOQs (from 20 pcs for tubes, 10 pcs for valves, master-carton spools for tapes), protected by DDP, FOB, and CIF terms.
Our expansive 2,000+ square-meter operating and production facility employs automated slit-winding equipment, optical defect scanning, and multi-stage pressure decay verification chambers. By optimizing manufacturing throughput and standardizing high-grade raw components, we protect overseas distributors against global raw material price swings, delivering steadfast pricing stability year after year.
Frequently Asked Questions: Sourcing Tubeless Rim Tape for the UK Market
Essential trade, technical, and regulatory answers for Liverpool bike builders, workshop owners, and e-commerce brand buyers.
What is the optimal tape width for modern asymmetric tubeless rims?
As a rule of thumb for modern hooked or hookless rims, select a tape width that is 2mm to 4mm wider than the internal rim channel width. For instance, an internal width of 25mm requires a 27mm or 29mm tape to properly line the central channel depression and seal up to the bead wall without interfering with tire lock.
How does your tape withstand low-temperature storage in UK winter conditions?
Our cross-linked solvent acrylic adhesive formulation retains ductile adhesion down to -25°C. It resists the glass-transition embrittlement typical of cheap hot-melt rubber adhesives, preventing spontaneous edge-flaking during frigid unheated warehouse storage or winter riding in Northern England.
Do you support OEM branding, custom widths, and retail packaging?
Yes. Our in-house technical and branding team supports custom core printing, bespoke backing-liner branding, custom die-cut circular valve repair dots, and full blister/retail cardboard box execution tailored for British cycling brands and shop chains.
What are the accepted payment structures and logistics terms for UK buyers?
We support standard B2B terms including T/T, L/C, PayPal, and credit card payments across GBP (£), EUR (€), and USD ($). Freight shipping options include direct air express for emergency restocking, air cargo, and ocean containerized DDP/CIF routing into Liverpool and Southampton.