High-Performance Components & Essential Hardware
Engineered for endurance and extreme reliability across Flemish pavé and European urban thoroughfares. Direct manufacturer pricing with flexible B2B minimum order quantities.
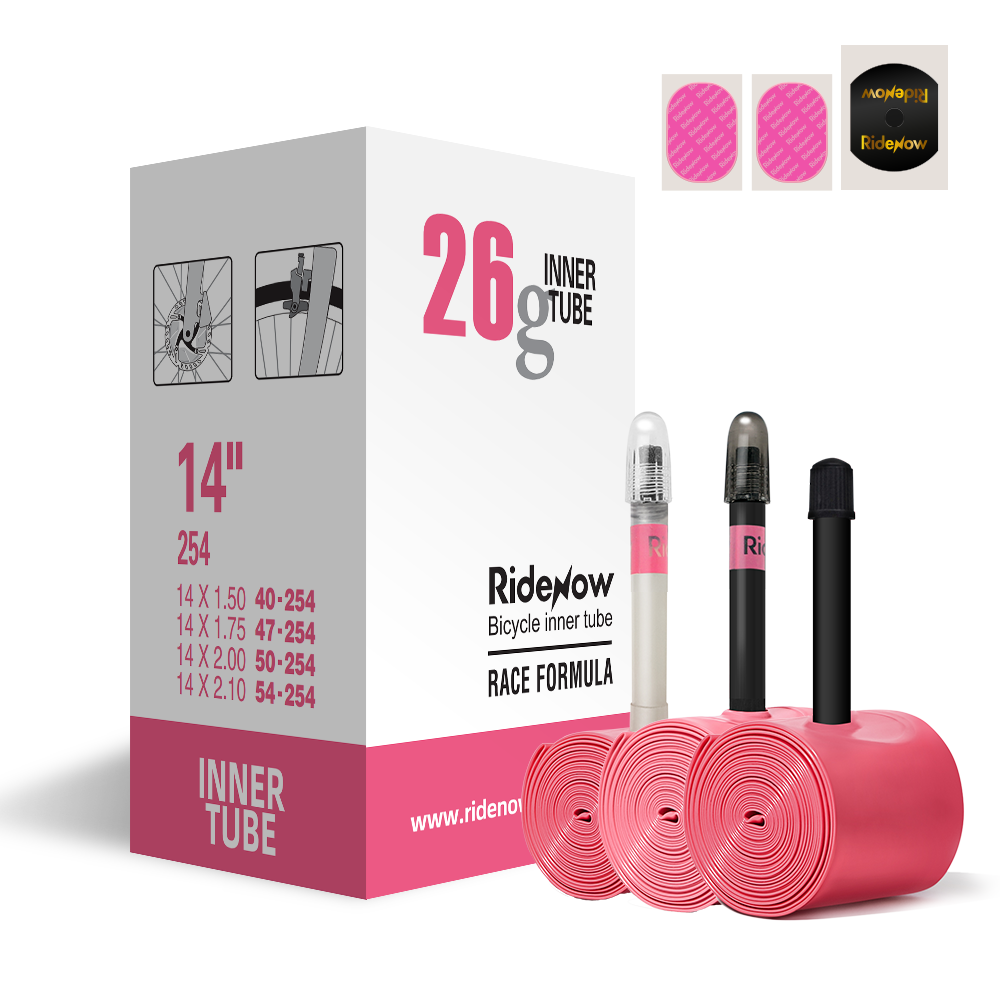
RideNow Kids Bike TPU Tube 14" Presta/Schrader
- Dimensions: 14" 254 (1.3–2.0")
- Valve: Presta / Schrader Option
- Puncture-resistant TPU compound
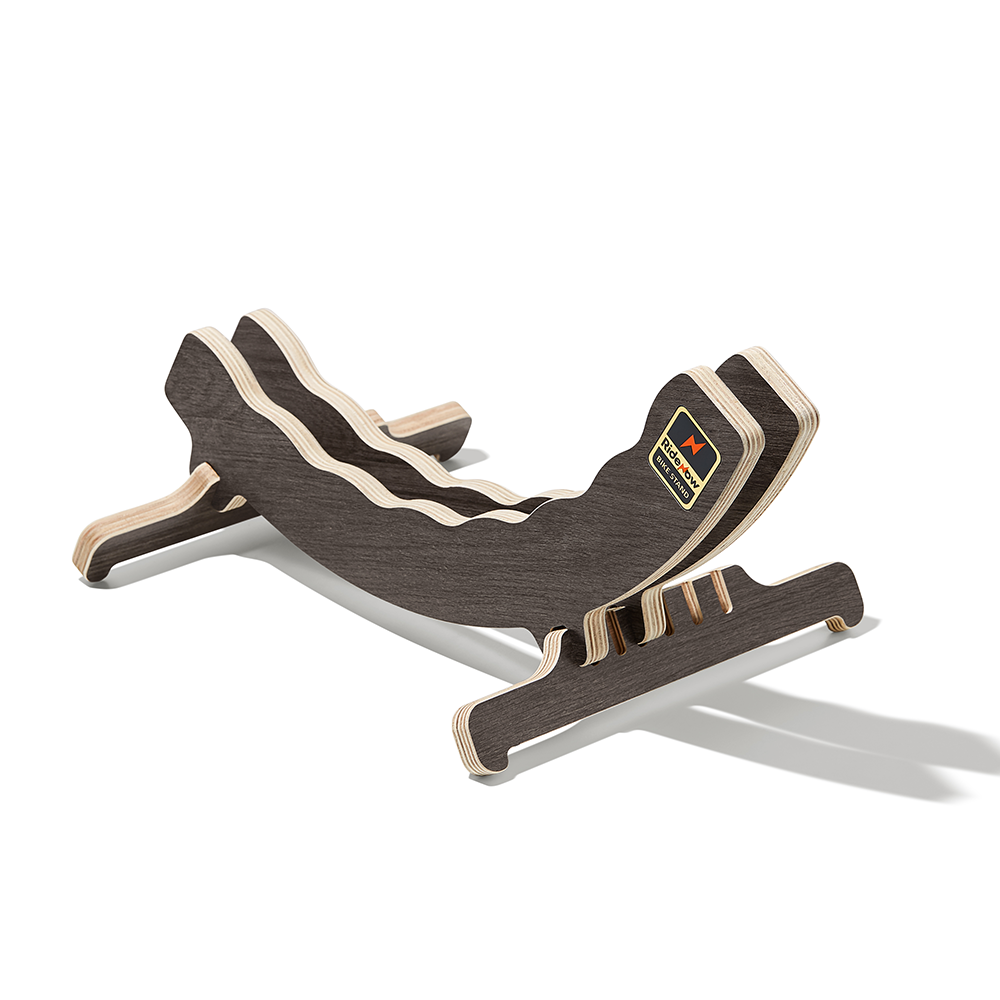
RideNow Wooden Bike Stand E0 Grade Plywood
- Multi-wheel width compatibility
- Eco-certified E0 plywood base
- Modular slot-together assembly
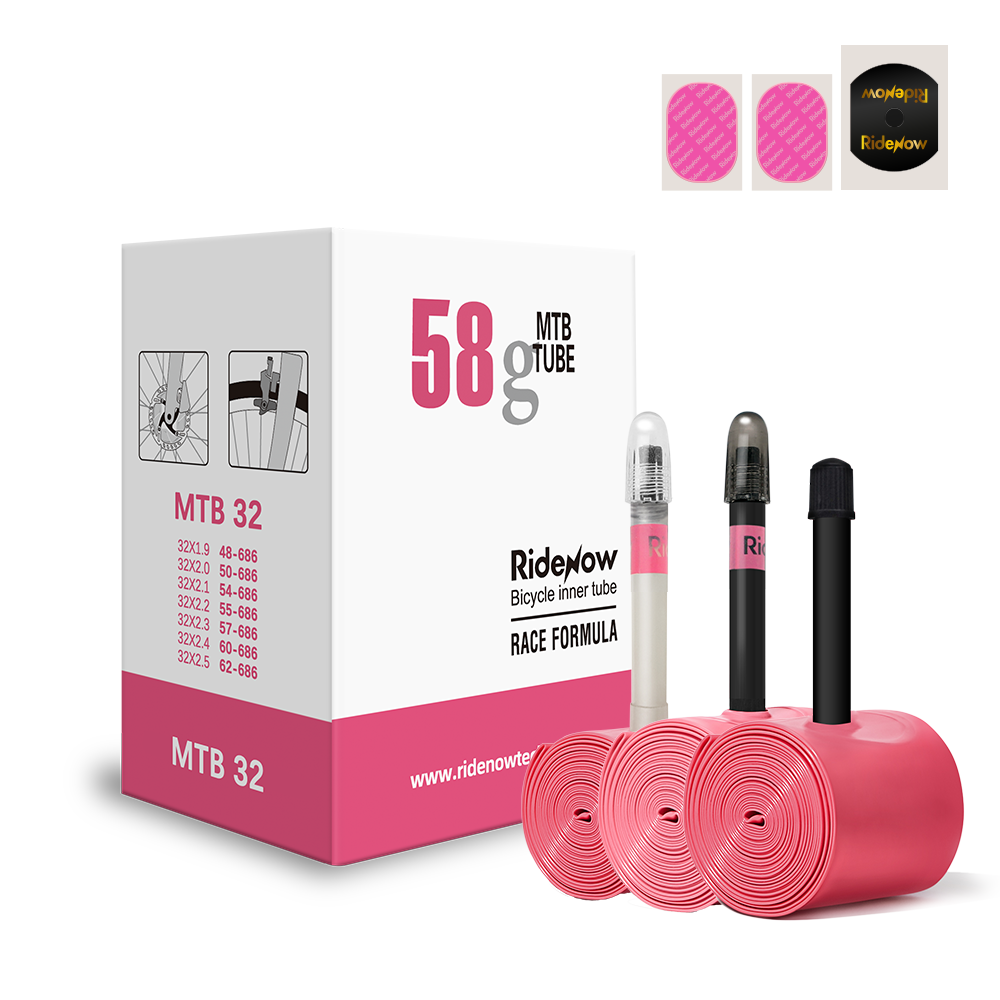
RideNow MTB TPU Repair Kit 45/65mm
- Reinforced patches for TPU walls
- Dedicated solvent-free adhesive pads
- Compact trail carry format
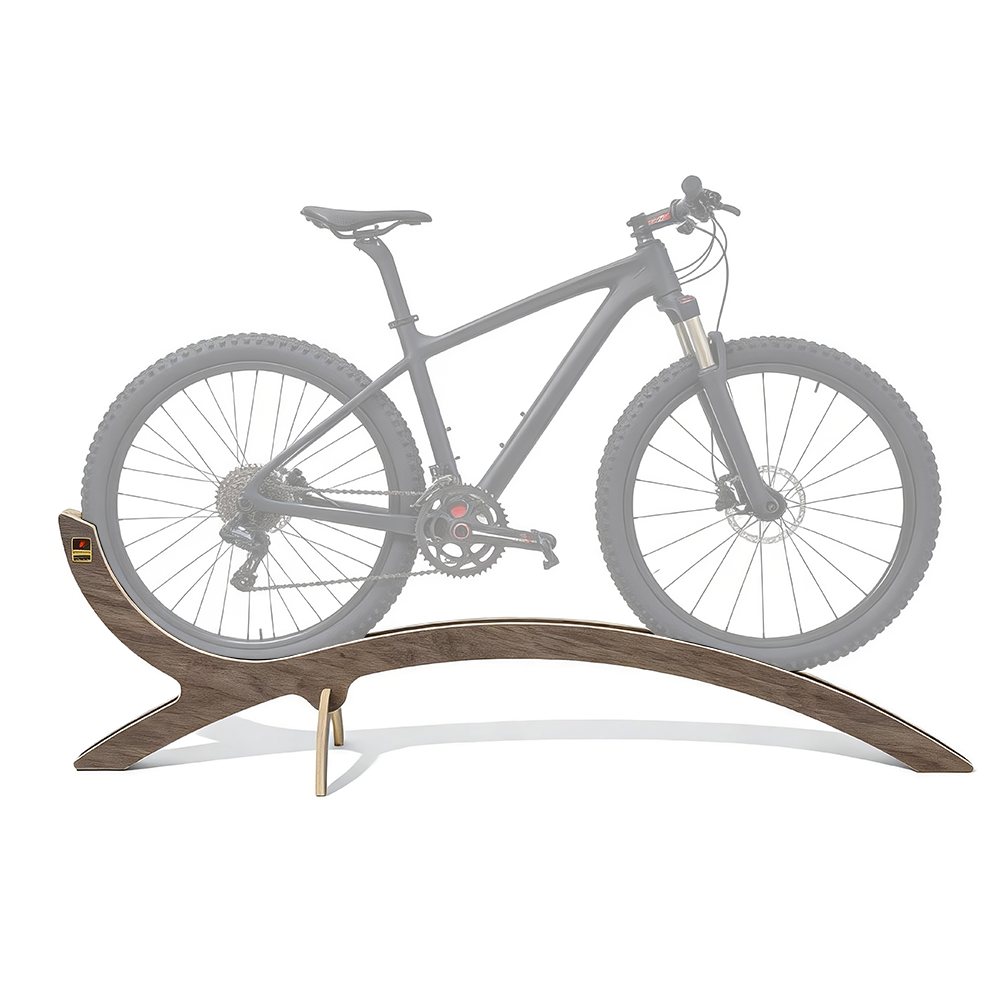
Bike Display Stand for Complete Bike Shows
- Heavy-duty load bearing capacity
- Customizable brand surface engraving
- Fits road, gravel, and heavy MTB
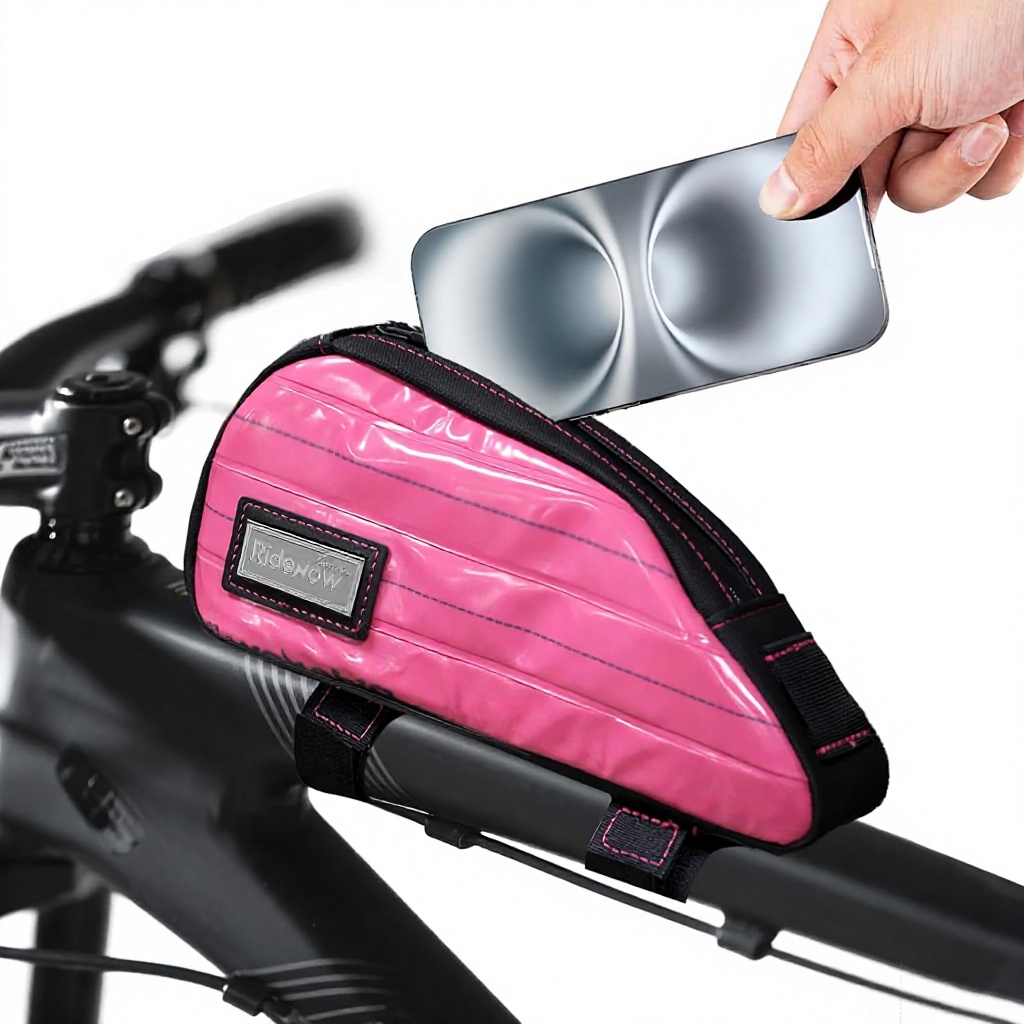
RideRow Compact Handlebar Bag 163g
- IPX5 Waterproof treated polyester
- Secure 3-point anti-sway mounting
- Fits up to 6.1" mobile displays
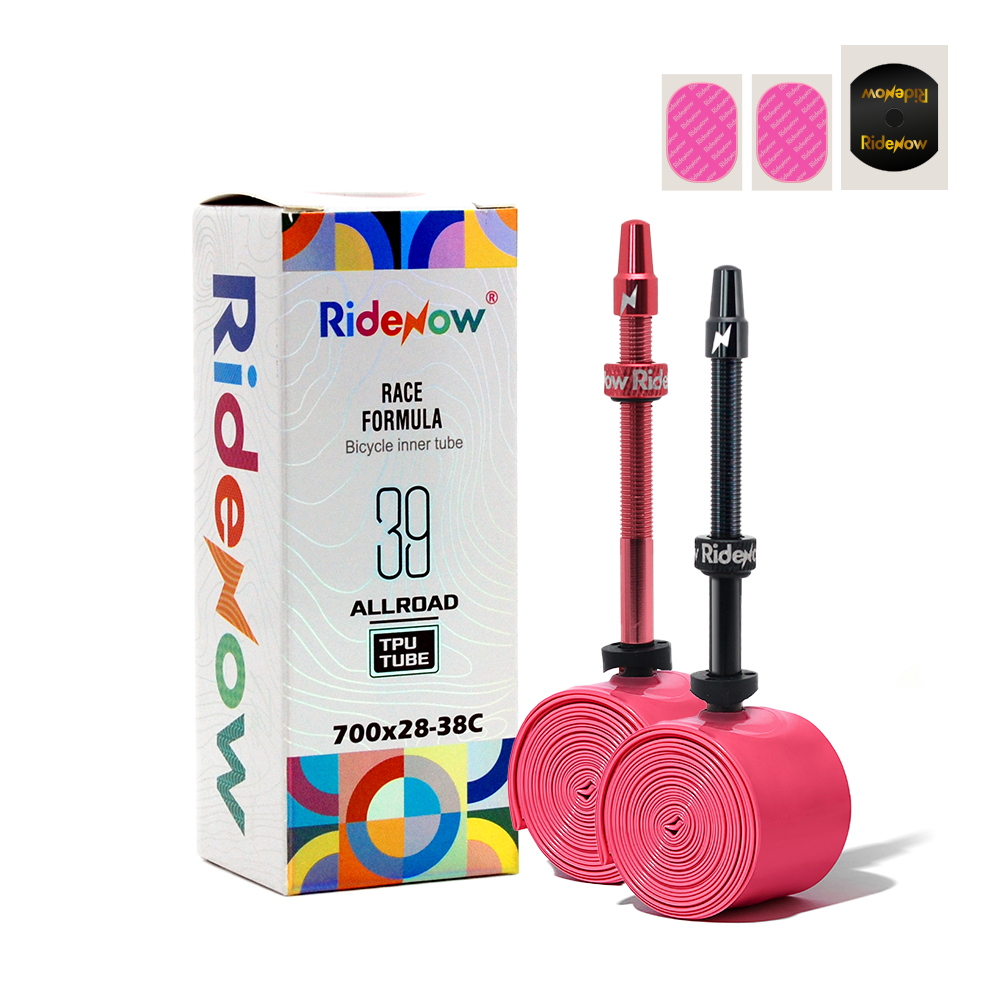
RideNow Road TPU Tube 700x28–38C
- Alloy Presta stem: 45 / 65 / 85mm
- Optimized for wider gravel/road tires
- Ultralight rolling resistance
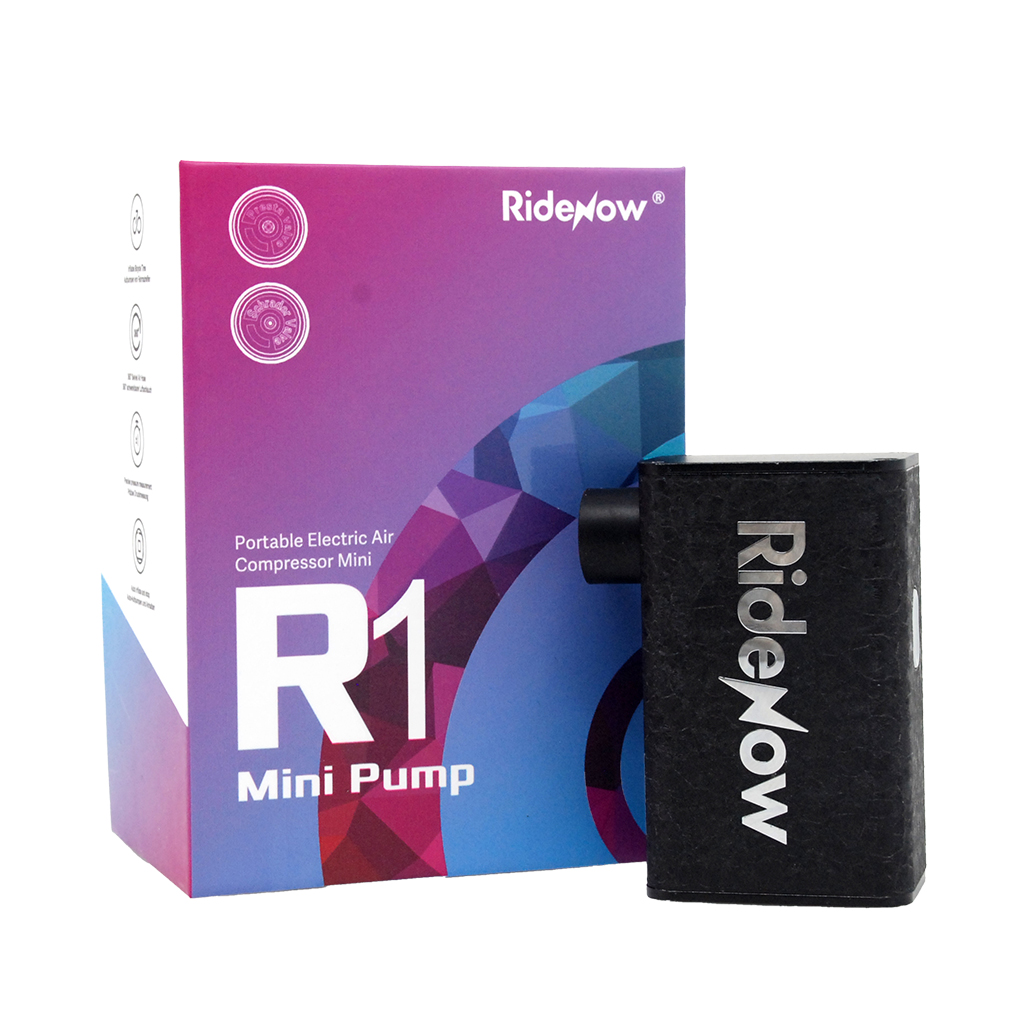
RideNow Mini Aluminum Pump R1S Auto-Stop
- Max pressure: 8.27 bar / 120 PSI
- Integrated digital manometer
- CNC 6063 aerospace alloy casing
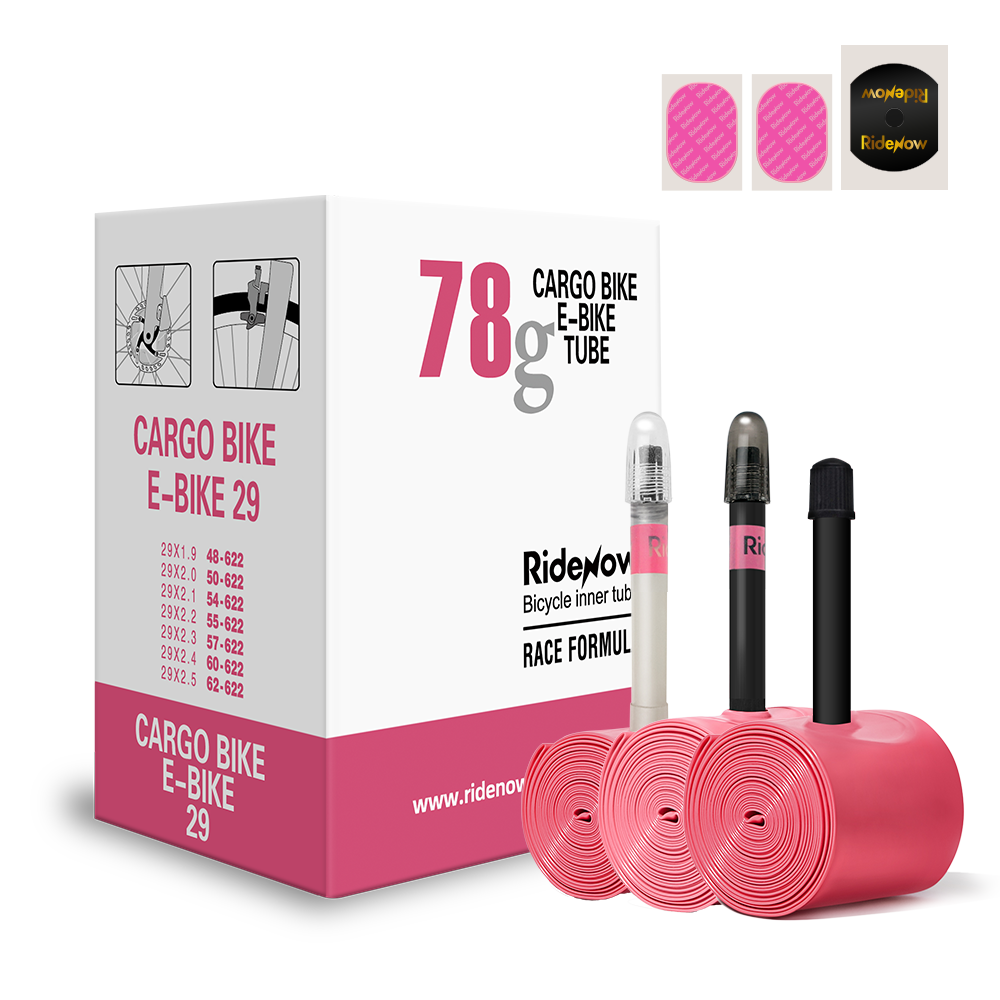
RideNow Heavy-Duty Cargo TPU Tube 29"
- Engineered for high cargo payload
- Tire cross-section: 1.9–2.5"
- Reinforced air retention membrane
High-Yield Tubeless Valve Stems: Fluid Dynamics & Metallurgical Integrity
A rigorous examination of tubeless valve stem design, alloy specifications, and sealing dynamics engineered to withstand severe cobble-impact vibration and corrosive municipal road salts.
In modern cycling mechanics, tubeless tire systems have superseded tubular and conventional inner tube systems across both competition and commercial transportation sectors. However, the pneumatic integrity of a tubeless rim-tire interface relies fundamentally upon a single critical component: the tubeless valve stem. For professional bike shops, racing workshops, and commercial logistics operators across Lille, Roubaix, and the greater Hauts-de-France region, valve stem failure represents the leading cause of pressure drops, sealant crystallization failure, and unseated tire beads.
Standard commercial valve stems frequently utilize nickel-plated brass or cast 6061 aluminum alloy. While cost-effective for basic production, these materials display significant operational liabilities when exposed to intense pavé vibration and modern high-pressure tubeless setups. Brass confers an undesirable rotational weight penalty at the rim perimeter, amplifying the rotational moment of inertia. Conversely, standard 6061 cast alloys often feature microscopic void porosity, rendering the stem vulnerable to thread shearing under hand-pump leverage or catastrophic snapping during rocky trail strikes.
Qingdao JORV Technology Co., Ltd. addresses these engineering challenges through high-precision CNC micro-milling of cold-forged aerospace-grade 7075-T6 aluminum alloy. This structural grade delivers double the tensile strength of common aluminum alloys while drastically shaving mass. Furthermore, the fluid dynamics of our valve bore have been fundamentally re-engineered. By expanding the internal lumen diameter by 28% compared to standard Presta cores and implementing four lateral multi-port base channels, our valves permit high-volume laminar airflow. Mechanics can rapidly seat tight tubeless beads utilizing standard shop floor pumps without requiring industrial air accumulator tanks, while sealant can be injected cleanly without clogging the stem conduit.
7075-T6 Cold-Forged Alloy
Unmatched fatigue tolerance and sheer resistance against rim-hole impact forces. Chemically passivated and anodized to resist winter road de-icing agents and humid French climates.
Omni-Port Base Dynamics
Engineered base channels eliminate tire-insert airflow blockages. Guarantees unobstructed fluid flow during high-viscosity sealant injection and instantaneous tubeless bead pop.
Universal Grommet Geometry
Features swappable vulcanized dual-density conical and square rubber bases. Ensures zero-leak hermetic sealing across asymmetric carbon aero rims and traditional hooked alloy profiles.
Optimized for the Demands of Lille & Northern European Cycling
From the cobbled sectors of Paris-Roubaix to urban municipal delivery hubs across the MEL (Métropole Européenne de Lille), our equipment serves distinct logistical and mechanical profiles.
01. Pavé & Endurance Gravel
The notorious sectors of Mons-en-Pévèle and Roubaix subject wheelsets to severe mechanical shock. Our 7075 valve stems feature contoured O-ring locking collars that do not back off under extreme resonance, preventing bead unseating on loose stone paths.
02. Urban Fleets & E-Cargo Logistics
Lille’s low-emission zones (ZFE-m) have triggered a massive surge in commercial e-cargo fleets along the Deûle canal. Tubeless valve assemblies and reinforced TPU cargo inner tubes ensure zero pinch flats under 200 kg gross transport loads, slashing delivery downtime.
03. Year-Round All-Weather Commuting
Operating under typical Nord-Pas-de-Calais oceanic weather conditions characterized by prolonged rainfall and freezing winter slush. Our hard-anodized valve caps with integrated valve core removers prevent salt corrosion and grit contamination inside the core mechanism.
Northern European Market Trends Shaping B2B Component Sourcing
Strategic procurement shifts across France, Belgium, and Germany indicate a departure from disposable components toward modular, serviceable, and sustainable cycling systems.
The bicycle component supply landscape across Western Europe is experiencing a decisive architectural pivot. Three primary vectors dictate the purchasing policies of leading regional distributors and independent bike shop cooperatives:
1. Universal Integration with Synthetic and Eco-Friendly Sealants: Traditional ammonia-rich latex sealants are rapidly being regulated out of municipal fleets and eco-conscious workshops across France due to environmental and volatile organic compound concerns. Newer synthetic latex and plant-based fibrous sealants possess higher dynamic viscosity. Consequently, valve stems featuring narrow internal tapers suffer chronic clogging during top-ups. Modern procurement managers in Lille prioritize wide-bore Presta architectures that accommodate fibrous particles up to 1.5 mm without flow restriction.
2. Hookless Carbon Rim Standard Compliance: As carbon road and gravel wheel manufacturers adopt hookless (straight-side) rim profiles to reduce manufacturing waste and optimize aerodynamic tire-rim transitions, tolerance precision becomes unforgiving. Rim internal beds have shallower, sharper center channels. Valve stems must utilize flexible, micro-contoured elastomer grommets that settle into tight channels without distorting rim tape edges, thereby preventing micro-fissures and pressurized air bleed into hollow carbon rim cavities.
3. The Rise of TPU Hybrid Systems: Even within dedicated tubeless fleets, professional support teams and long-range commuters maintain emergency tubes. Traditional butyl tubes are too cumbersome, heavy, and susceptible to ozone degradation. Ultralight thermoplastic polyurethane (TPU) tubes, as engineered by JORV and RideNow, take up 70% less pack volume while delivering rolling resistance metrics competitive with pure tubeless configurations. This has generated immense wholesale demand for complementary displays featuring both premium tubeless valves and ultralight TPU emergency spares.
Engineering Parameter Comparison Matrix
Quantitative validation comparing standard market OEM components against our proprietary 7075-T6 aluminum tubeless Presta systems.
| Specification Feature | Standard Brass OEM | Generic 6061 Alloy | JORV / RideNow 7075-T6 Alloy | Procurement Advantage |
|---|---|---|---|---|
| Tensile Yield Strength | ~250 MPa | ~275 MPa | 505–540 MPa Superior | Resists severe impact shear & leverage bending |
| Unit Mass (45mm Stem) | 16.8 g / piece | 6.2 g / piece | 4.1 g / piece Ultralight | Reduces high-speed rotational wheel imbalance |
| Internal Lumen Bore | 3.2 mm standard | 3.4 mm standard | 4.2 mm Oversized +28% Flow | Instantaneous high-volume tubeless bead seating |
| Sealant Clog Resistance | Moderate (Straight cut) | Moderate (Straight cut) | High (Multi-Port Lateral Slots) | Prevents core clogging with fibrous sealants |
| Anodizing Coating Depth | None (Nickel-plate) | 5–8 μm decorative | 15 μm Hard-Anodized | Withstands aggressive winter road de-icers |
| Rim Bed Compatibility | Rigid Conical only | Conical only | Dual Conical + Square Grommets | Universal fit across alloy, carbon & hookless |
Why Global B2B Brands Partner with Qingdao JORV Technology
Direct access to vertically integrated manufacturing, European-based industrial design, and an agile international supply chain network.
Founded on R&D Rigor
Established in 2017 by cycling-obsessed engineers. We hold over 12 self-developed product lines spanning wheel balancers, indoor cycling platforms, and advanced TPU pneumatic solutions.
30%+ R&D Reinvestment
We reinvest over thirty percent of annual corporate profits into advanced materials testing, automated tooling upgrades, and aerodynamic fluid flow modeling.
Düsseldorf Design Center
Our research and development center in Düsseldorf, Germany, coordinates directly with European cycling standards to ensure DIN EN ISO 4210 compliance across all product batches.
Global Logistics Agility
With operational facilities in Qingdao, branching in Shenyang, and supply-chain management in Taiwan, we deliver rapid sample fulfillment and full-container DDP export to Western Europe.
Frequently Asked Questions by European Sourcing Managers
Essential operational details regarding logistics, customs clearance, minimum quantities, and technical specifications for Hauts-de-France distributors.
To support independent regional shops, service centers, and testing programs, our entry MOQ for tubeless valve stems begins at just 10 pieces (or retail pair packs). For our ultralight TPU bike inner tubes, standard MOQ is 20 pieces per size, allowing distributors to curate complete wheel-size assortments without substantial capital lockup.
Yes. We regularly supply European accounts via FOB, CIF, EXW, and comprehensive DDP arrangements. Under DDP terms, all French import customs formalities, VAT processing, and maritime/air cargo tariffs are completely handled prior to final truck dispatch directly to your warehouse dock in the Hauts-de-France region.
Our valve bases are engineered with a 4-channel cross-cut multi-port foundation. When run in conjunction with closed-cell EVA or polyurethane tire inserts common in gravel and downhill racing, the insert sits securely atop the valve base without choking off the air channel or inhibiting pressure sensor readings.
Yes, our Qingdao production and Taiwan supply chain teams provide extensive white-label and private-label programs. We support custom Pantone-matched hard anodizing (including team editions: matte black, petroleum oilslick, race red, anodized violet), custom laser logo engraving on lock rings, and retail-ready hanging card blister packaging.
We supply standard production lengths of 45 mm (ideal for low-profile alloy and shallow gravel rims up to 28 mm depth), 65 mm (engineered for mid-depth aero sections 35–45 mm), and 85 mm (for deep-dish carbon wheels up to 65 mm). Custom extensions and valve stem lengths up to 100 mm are available on special OEM production runs.
We facilitate transactions in EUR, USD, GBP, CHF, and other major currencies via secure international Wire Transfer (T/T), Letter of Credit (L/C), Credit Card, and PayPal. Standard production payment schedules for volume OEM orders include structured 30% advance deposit with balance cleared against Bill of Lading (B/L) documentation.