Featured Precision Valve & Inner Tube Products
Engineered for competitive cycling, tubeless conversions, and high-performance tire pressure management systems.
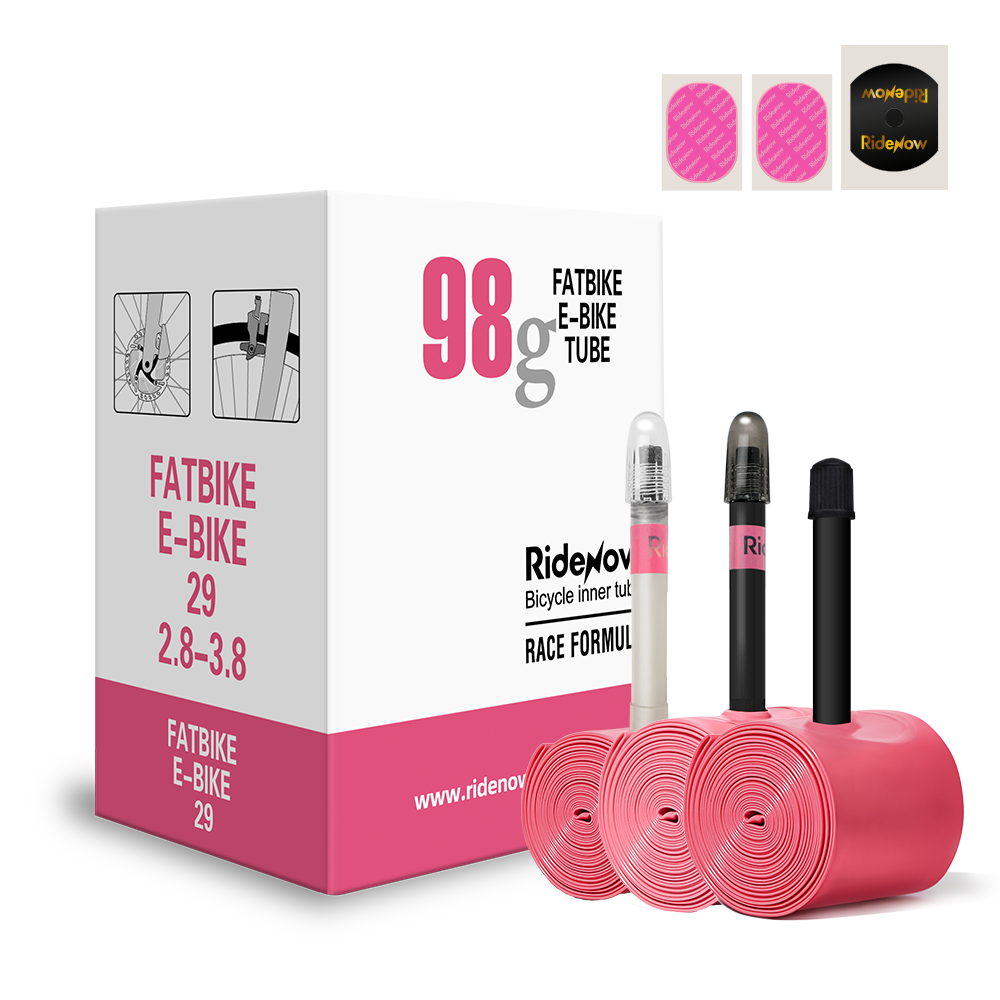
RideNow FAT Bike Inner Tubes Presta/Schrader 29" 2.8-3.8
View Details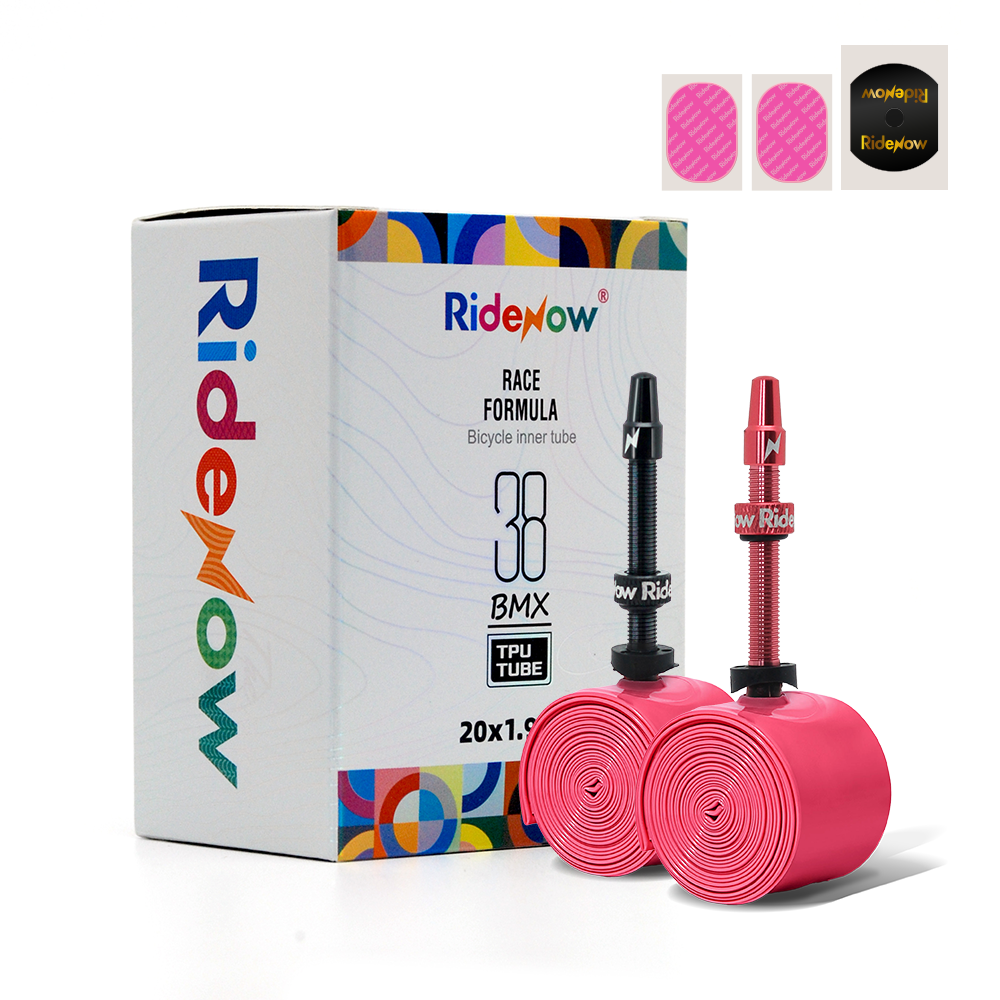
RideNow BMX Bike TPU Inner Tube 20" Presta Metal Valve 45mm
View Details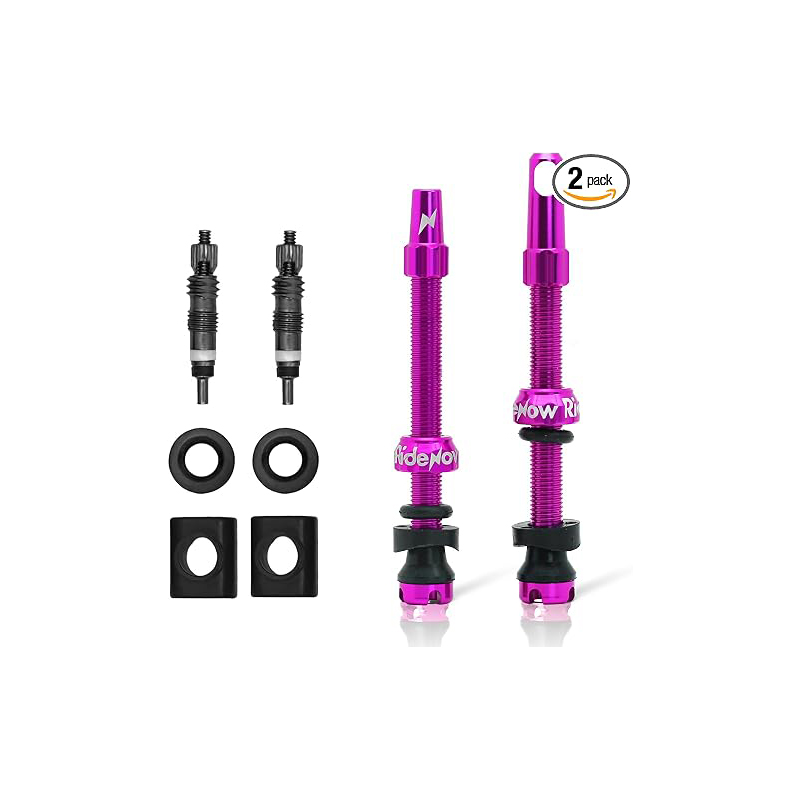
RideNow Tubeless Presta Valve Stems 7075 Aluminum Purple Pair
View Details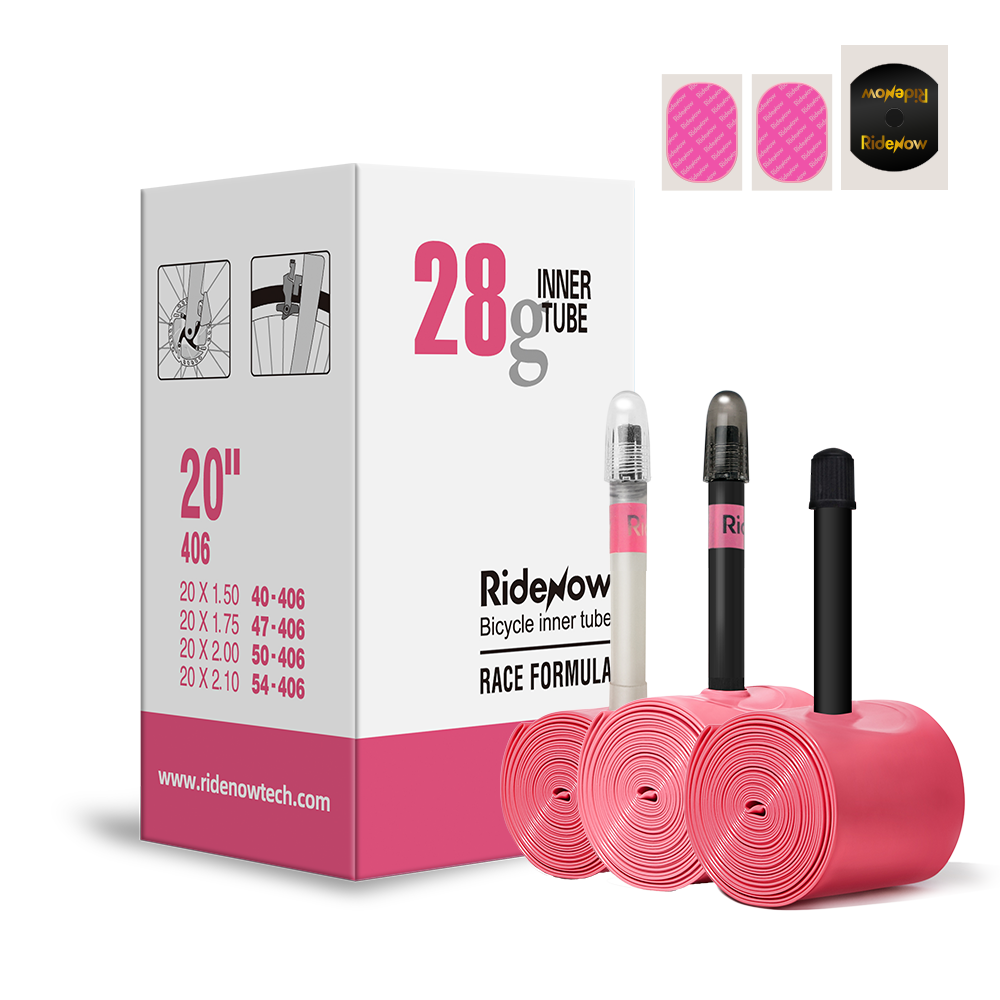
RideNow Folding Bike TPU Inner Tube 20" Presta/Schrader 1.3-2.0
View Details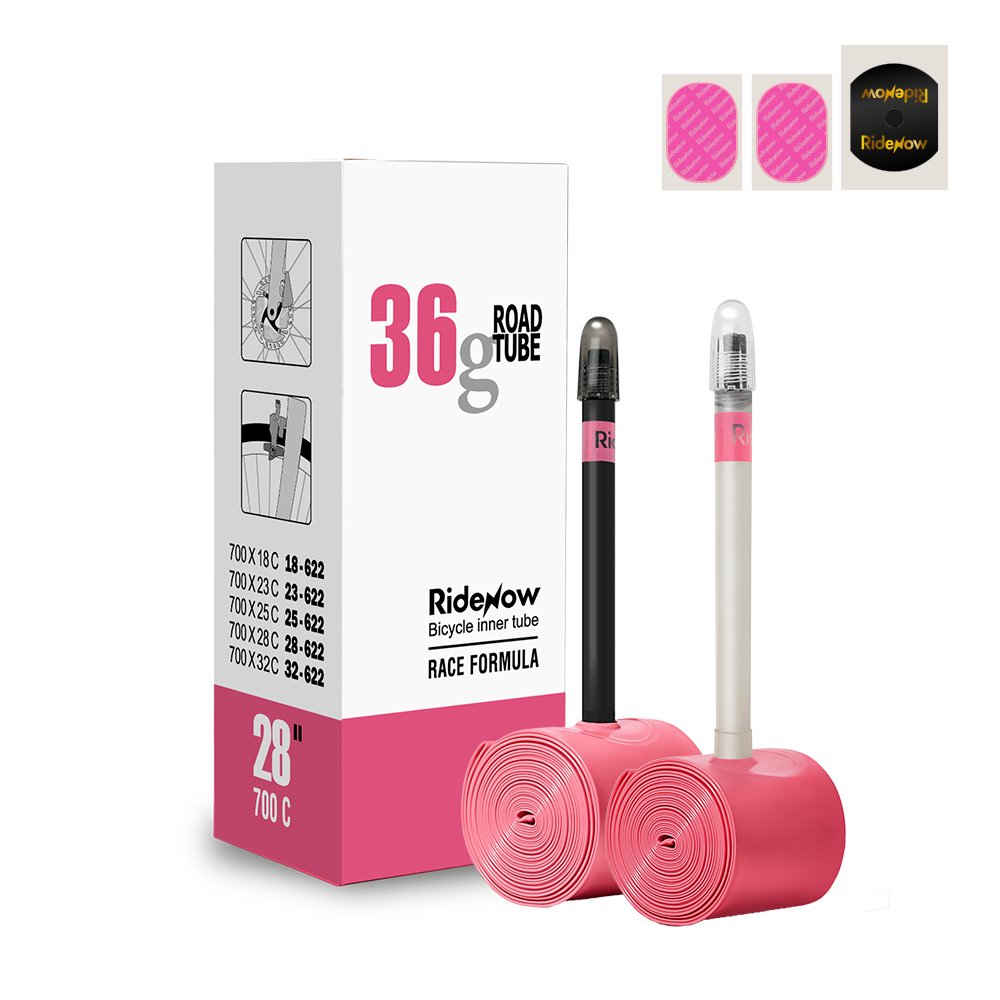
RideNow Road Bike Inner Tubes 700x18-32C TPU Presta Valve 36g
View Details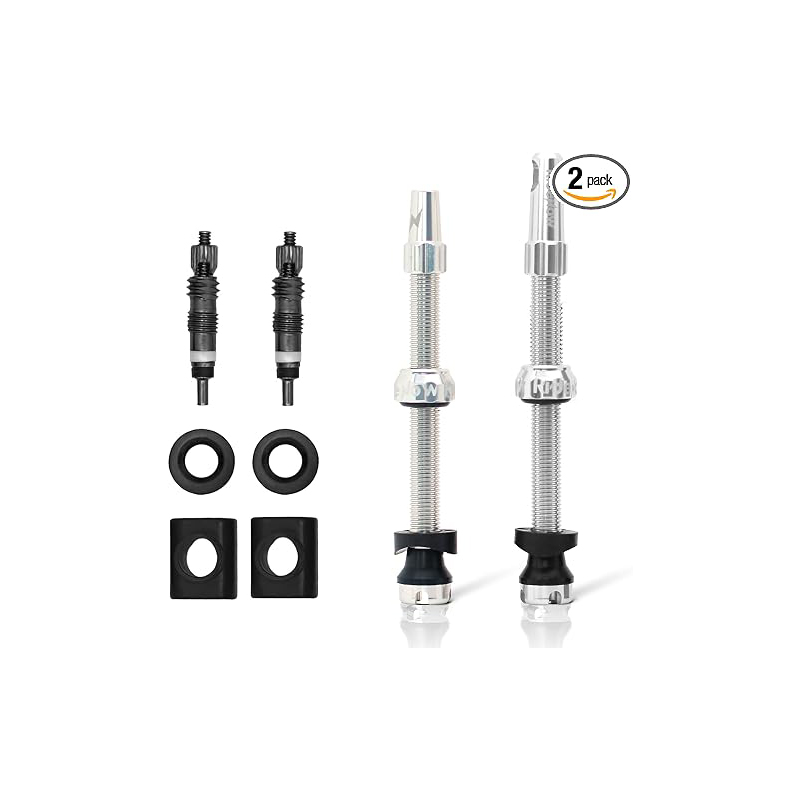
RideNow Tubeless Presta Valve Stems 7075 Aluminum Silver Pair
View Details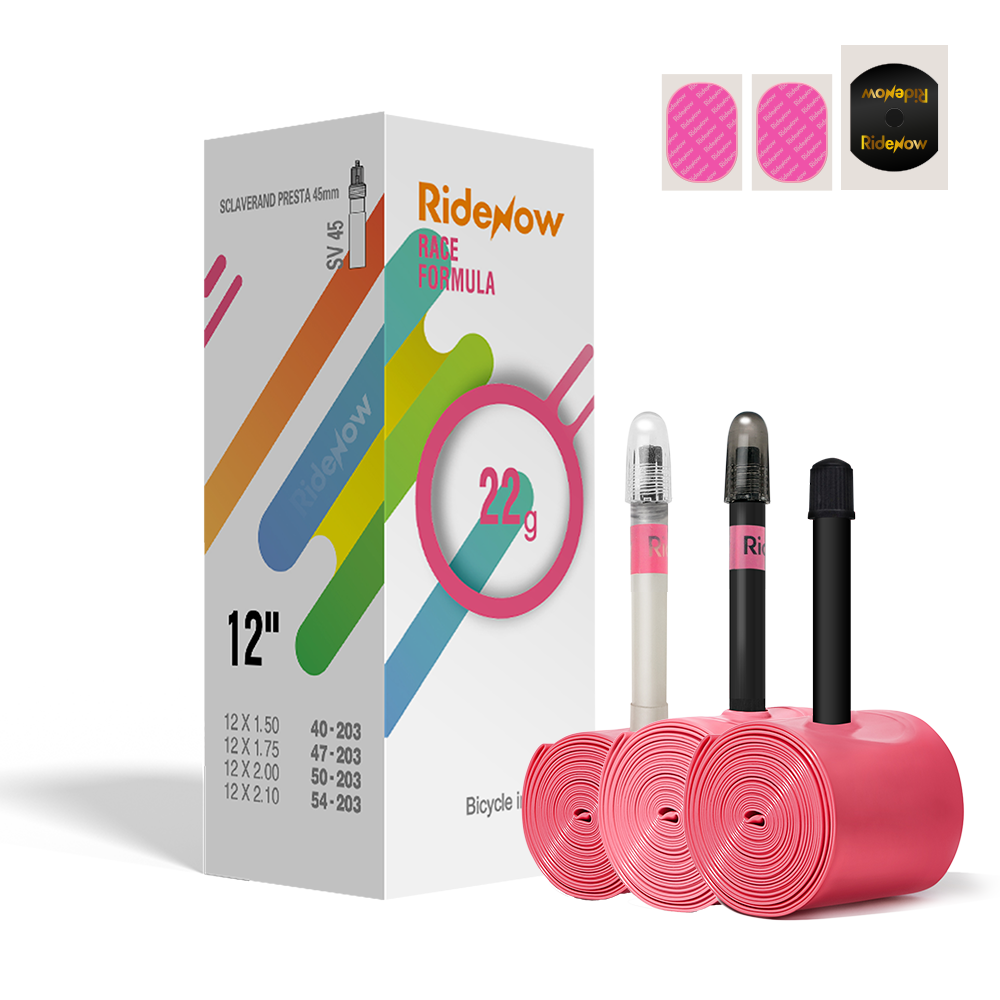
RideNow Kids Bike TPU Inner Tube 12" 203 Presta/Schrader
View Details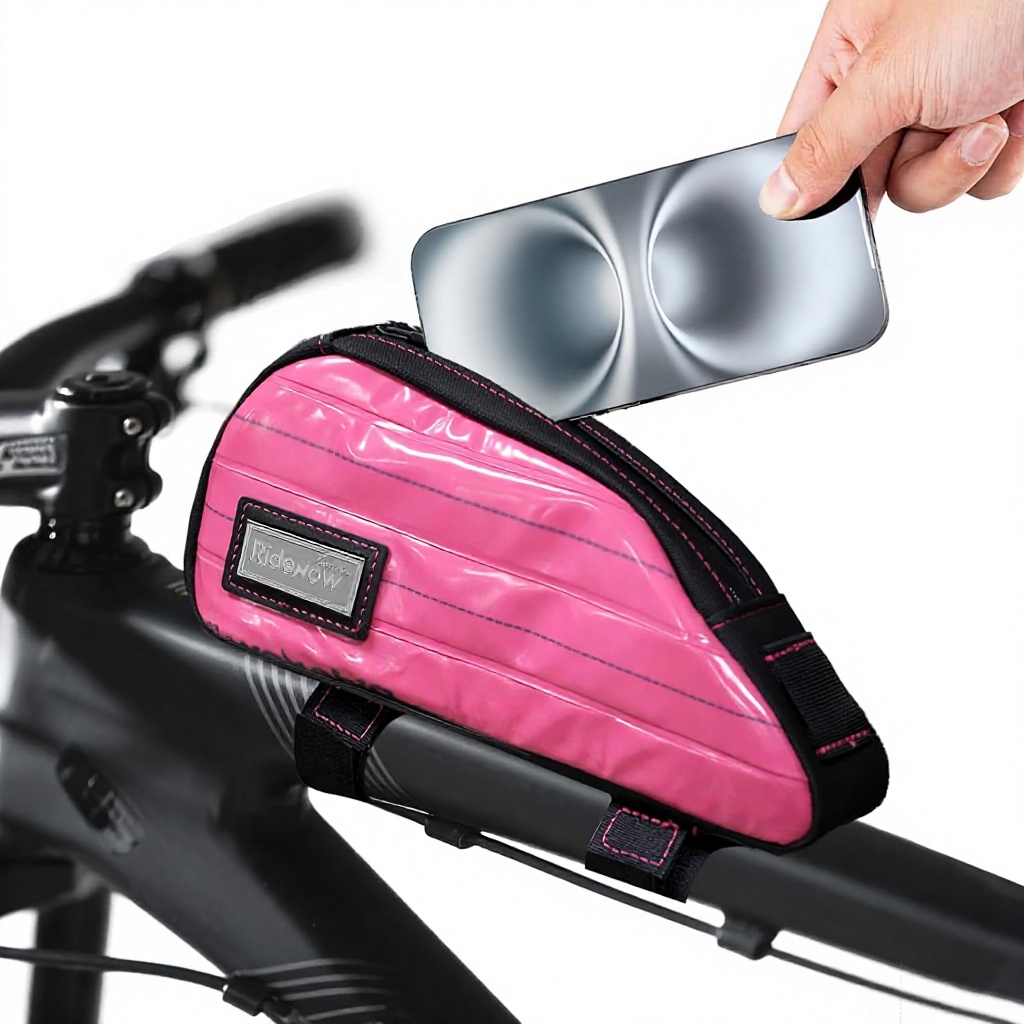
RideRow Compact Bike Handlebar Bag Waterproof Polyester 163g
View DetailsExecutive Sourcing Analysis: Sourcing High-Precision Valve Core Removers
In modern pneumatic inflation infrastructure—spanning high-end road racing bicycles, heavy-duty commercial vehicles, HVAC service apparatus, and aerospace pressure seals—the integrity of the valve interface relies entirely on the mechanical interface between the valve core and the stem housing. A valve core remover is not merely a hand tool; it is a critical calibration instrument designed to apply exact rotational torque without galling aluminum threads, compromising O-ring elastomer seals, or distorting brass valve pins.
For global B2B procurement managers, brand directors, and bicycle component distributors, sourcing from top trusted valve core remover manufacturers & factories requires a technical auditing approach. The modern market is undergoing a paradigm shift: driven by the rapid global adoption of tubeless tire setups, liquid sealant injection procedures, and ultralight TPU (Thermoplastic Polyurethane) inner tube integration, the demand for precision CNC-machined, multi-functional valve tools has reached an all-time high.
The Information Gain Metric: Material Integrity & Tolerance Control
Unlike standard stamped steel or molded plastic promotional tools that strip under 0.5 Nm of torque, premium OEM valve core removers are machined from aircraft-grade 7075-T6 aluminum alloy. This material selection delivers a tensile strength exceeding 570 MPa—ensuring thousands of service cycles without widening the engagement slot or rounding the valve core flat flats.
Technical Benchmark Criteria for Evaluating Valve Core Tool Manufacturers
When auditing factory partners in major manufacturing hubs such as Qingdao, Ningbo, or Taichung, procurement officers must look beyond unit price to evaluate underlying metallurgical and machining standards. The following engineering metrics separate top-tier OEMs from low-grade suppliers:
Machining Tolerances (±0.01mm)
High-speed 5-axis CNC turning ensures the engagement slot perfectly matches standard Presta (VC-1) and Schrader (5V1) flat dimensions, eliminating slippage and core deformation during field repairs.
Anodization & Corrosion Resistance
Mil-Spec Type II anodization creates a 10–15 micron protective aluminum oxide layer. This prevents galvanic corrosion when tools interact with ammonia-based tubeless tire sealants or marine salt spray environments.
Ergonomic Knurling & Torque Control
Diamond-pattern or linear axial knurling delivers optimal tactile grip, enabling technicians to achieve precise hand-tight torque specifications (0.4 to 0.6 Nm) without risk of over-tightening.
Material Performance Matrix: Tool Metallurgy Comparison
Understanding raw material properties allows procurement teams to optimize cost-to-performance ratios based on target market positioning:
| Material Grade | Tensile Strength (MPa) | Corrosion Resistance | Weight Density (g/cm³) | Ideal Application Segment |
|---|---|---|---|---|
| 7075-T6 Aluminum Alloy | 570 MPa | Excellent (Anodized) | 2.81 | Professional Workshop & Premium EDC Retail |
| 6061-T6 Aluminum Alloy | 310 MPa | High (Anodized) | 2.70 | Standard OEM Bundles & Consumer Multi-Tools |
| Nickel-Plated C36000 Brass | 440 MPa | Moderate | 8.50 | Commercial Automotive & Heavy HVAC Service |
| Injection Molded Glass-Nylon | 160 MPa | Impervious | 1.45 | Ultra-Budget Mass Market Giveaway Kits |
Future Procurement Trends in Cycling Accessories & Valve Maintenance (2025–2030)
As the cycling industry transitions from legacy butyl rubber systems toward high-efficiency tubeless setups and ultra-lightweight TPU inner tubes, hardware procurement requirements are rapidly changing. Procurement buyers must align their catalog development with four macroeconomic and engineering trends:
1. Integration of Tubeless Valve Stem & Core Tool Ecosystems
Retail consumers and professional mechanics no longer seek standalone single-purpose tools. Modern demand is shifting toward integrated systems where the valve cap doubles as an emergency CNC core remover, or where tubeless valve stems (such as 7075 aluminum Presta stems) ship with color-matched multi-functional aluminum core tools included in the retail packaging.
2. Rapid Growth of Ultralight TPU Inner Tube Adoption
TPU inner tubes—pioneered by engineering-driven brands like RideNow—have revolutionized road, gravel, and mountain bike performance. Because TPU tubes utilize removable metal or specialized composite valve stems to maintain ultralight weight (down to 36 grams for 700C road tubes), precision core removal tools are required during installation to fit valve extenders for deep-section carbon rims without damaging delicate stem threads.
3. Sustainable Circular Sourcing & Anodization Waste Zero-Discharge
Leading brand owners in North America and Western Europe increasingly require supply chain audits covering environmental compliance. ISO 14001 certified factories utilizing closed-loop wastewater recovery for anodization baths and recycled aluminum billet stock are gaining a decisive competitive advantage in corporate bidding processes.
4. Custom Laser Engraving & Private Label Branding at Low MOQs
Traditional factory MOQs of 5,000+ units for custom tool manufacturing are giving way to flexible agile manufacturing models. Advanced factories utilizing automated fiber laser marking systems can offer customized logo engraving, custom Pantone anodization matches, and customized retail blister packaging at flexible order thresholds starting as low as 10 to 20 units for trial market testing.
Enterprise Advantage: Qingdao JORV Technology Co., Ltd.
At Qingdao JORV Technology Co., Ltd., we bridge the gap between high-precision mechanical engineering and scalable B2B manufacturing. Formed in 2017 by passionate cycling engineers, JORV has established a global operational footprint designed to provide B2B importers, distributors, and private-label brand owners with unprecedented engineering depth and supply chain stability.
- Global R&D Integration: Operating headquarters in Qingdao, China, supported by an advanced Research & Development hub in Düsseldorf, Germany, and supply chain management teams in Taiwan.
- 30%+ Reinvestment Rate: More than 30% of annual corporate profits are systematically reinvested into proprietary product development, automated CNC equipment, and precision quality testing apparatus.
- Agile Low MOQ Sourcing: To support brand incubator programs and distributor market testing, our minimum order quantities start at just 20 pieces for TPU inner tubes, 10 pieces for valve stem assemblies, and single-unit orders for specialized workshop equipment.
- Rapid Buyer Response SLA: Our dedicated technical sales team guarantees an average inquiry response time of under 13 hours, offering direct engineer-to-buyer consultation on thread specifications, custom packaging, and freight logistics (FOB, CIF, DDP, EXW).
Frequently Asked Questions (FAQ) for B2B Valve Core Remover Procurement
A dual-function professional valve core remover features two distinct slots: a narrower 4.5mm slot designed specifically to engage the flat sides of Presta valve cores (standard in road, gravel, and high-end MTB tubeless setups), and a wider 5mm slotted prong designed to fit Schrader valve cores (common in auto, E-bike, and heavy-duty utility applications). Multi-port workshop tools also integrate valve extension flats and thread-cleaning dies.
7075-T6 aluminum provides superior shear strength and hardness, preventing tool wear when removing valve cores that have become stuck due to dried latex sealant or over-torquing. Unlike molded plastic, CNC aluminum maintains exact dimensional tolerances under extreme thermal and mechanical conditions, guaranteeing a non-slip interface that protects expensive tubeless valve stems from damage.
Yes. We provide complete OEM/ODM customization services. Utilizing high-precision fiber laser marking machines, we can engrave company logos, part numbers, or torque specifications directly onto the anodized tool surface. Custom Pantone color anodizing (including anodized black, purple, red, blue, silver, and oil-slick finishes) is available for brand consistency.
Removing the valve core creates an unobstructed internal pathway through the valve stem housing, expanding the fluid aperture diameter. This allows high-viscosity liquid sealants containing sealing micro-fibers to be injected quickly without clogging the valve pin mechanism or causing sealant pressure blowbacks during installation.
Standard production lead time for stock components is 7–14 business days, while customized OEM orders typically ship within 20–25 days. We support flexible shipping terms including FOB Qingdao/Shanghai, CIF, EXW, and door-to-door DDP air/sea freight options with full customs clearance management.
Every batch undergoes rigorous ISO 9001 quality gates: key dimensions are verified using optical coordinate measuring machines (CMM), surface anodization thickness is measured via eddy-current testing, and random sample torque testing is conducted up to double the maximum recommended working limit to ensure zero mechanical failure rates in field conditions.
Partner with a Leading Valve Tool & TPU Tube Manufacturer
Access direct factory pricing, low minimum order thresholds, and world-class engineering support for your cycling accessory catalog.
Contact Us