Featured Precision Bicycle Components & Tools
Explore our CE-compliant, ultra-lightweight components and specialized maintenance tooling engineered for global distributors and high-performance workshop networks.
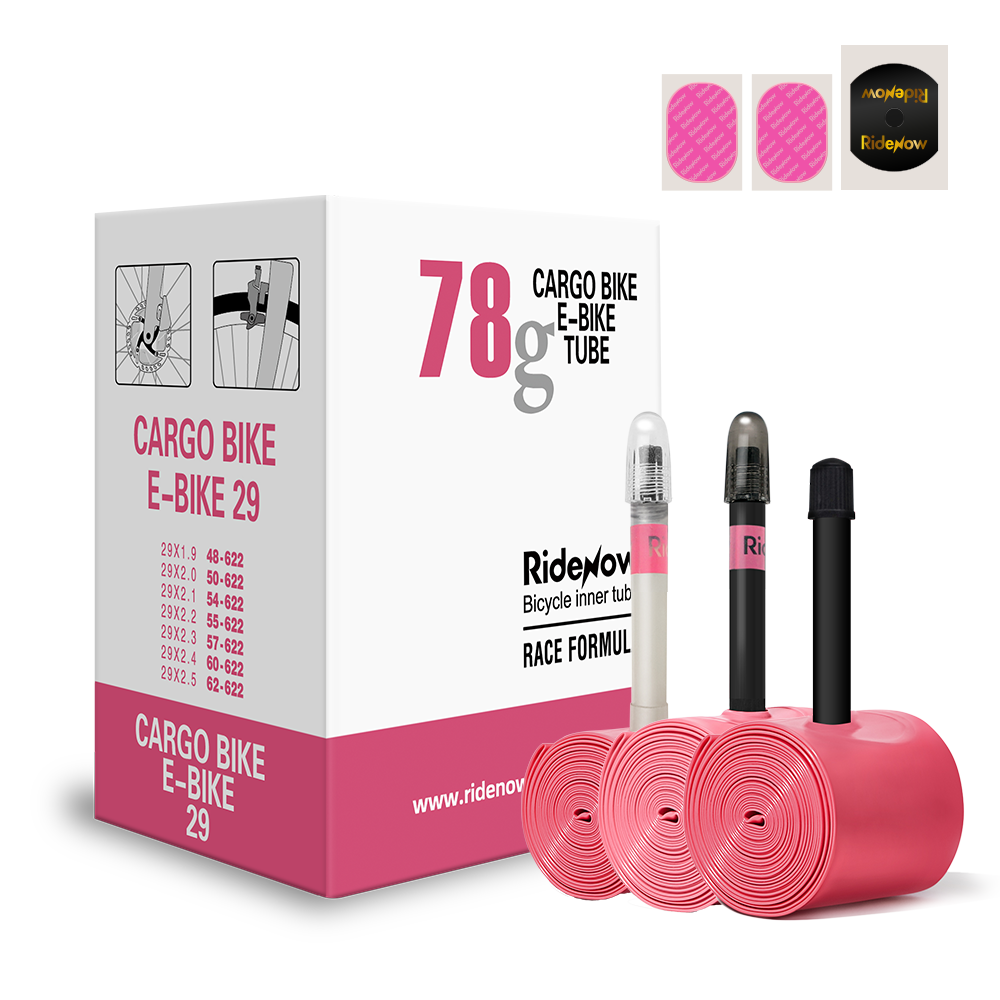
RideNow Cargo Bike Inner Tubes Presta/Schrader Valve 29Inch622 1.9-2.5 | Ultra-light Puncture-Resistant 45mm Patch Repair
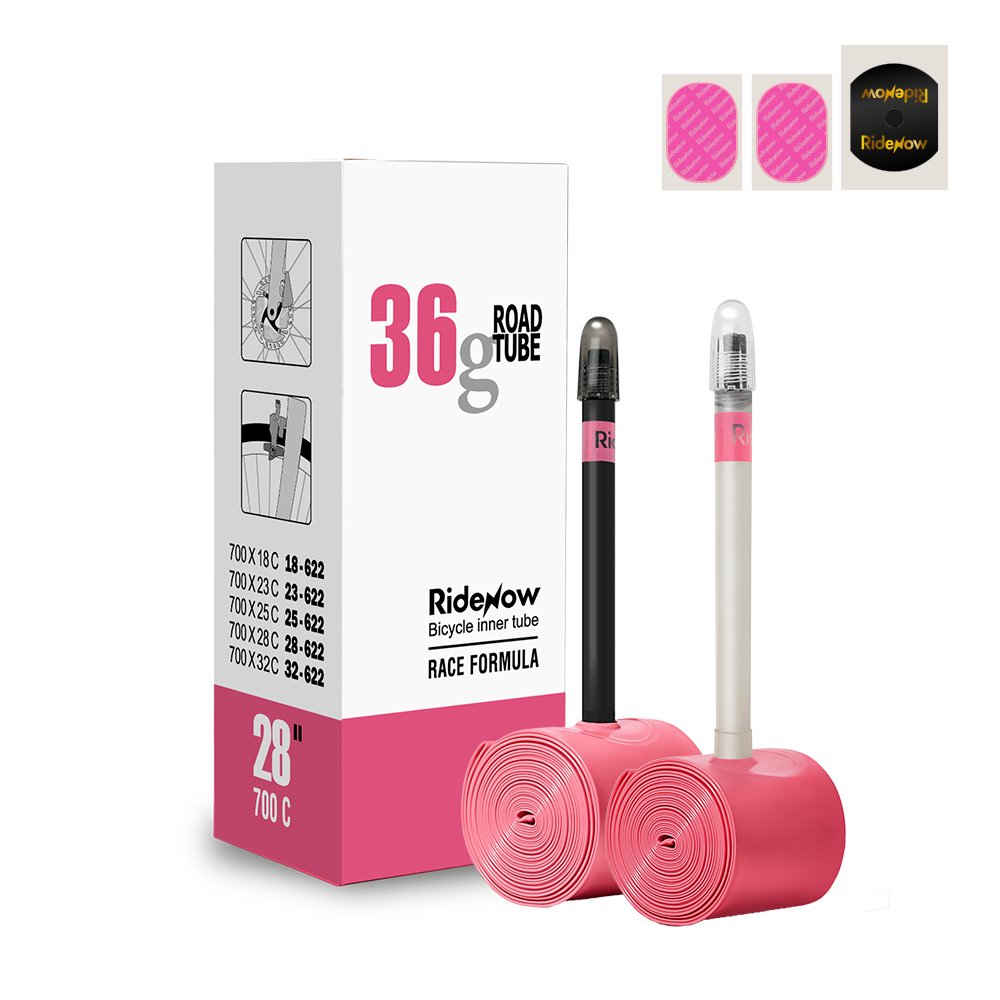
RideNow Road Bike Inner Tubes 700x18-32C TPU Presta Valve 36g Ultra-Light Puncture-Resistant Design Metal TPU Valve
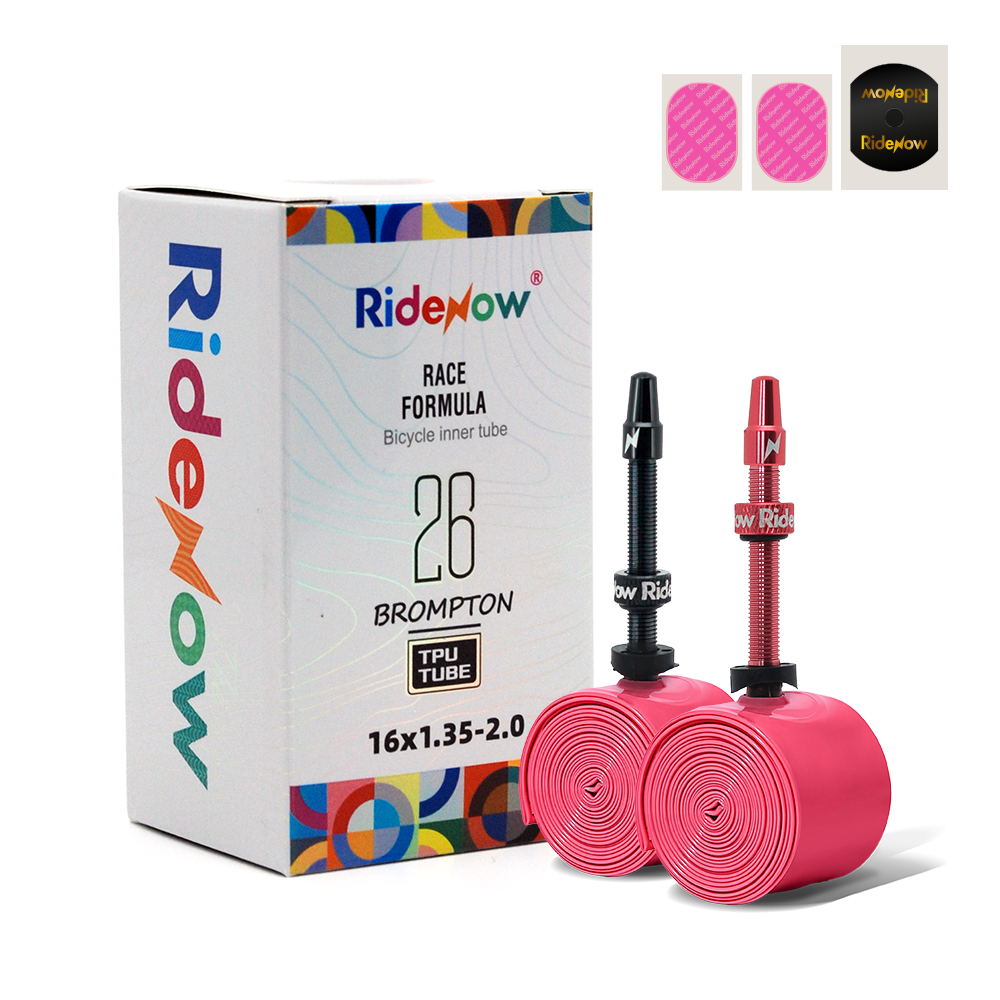
RideNow Folding Bike TPU Inner Tube 16/18" Metal Presta 349/355 | Ultra-light Puncture-Resistant Design Patch Kits
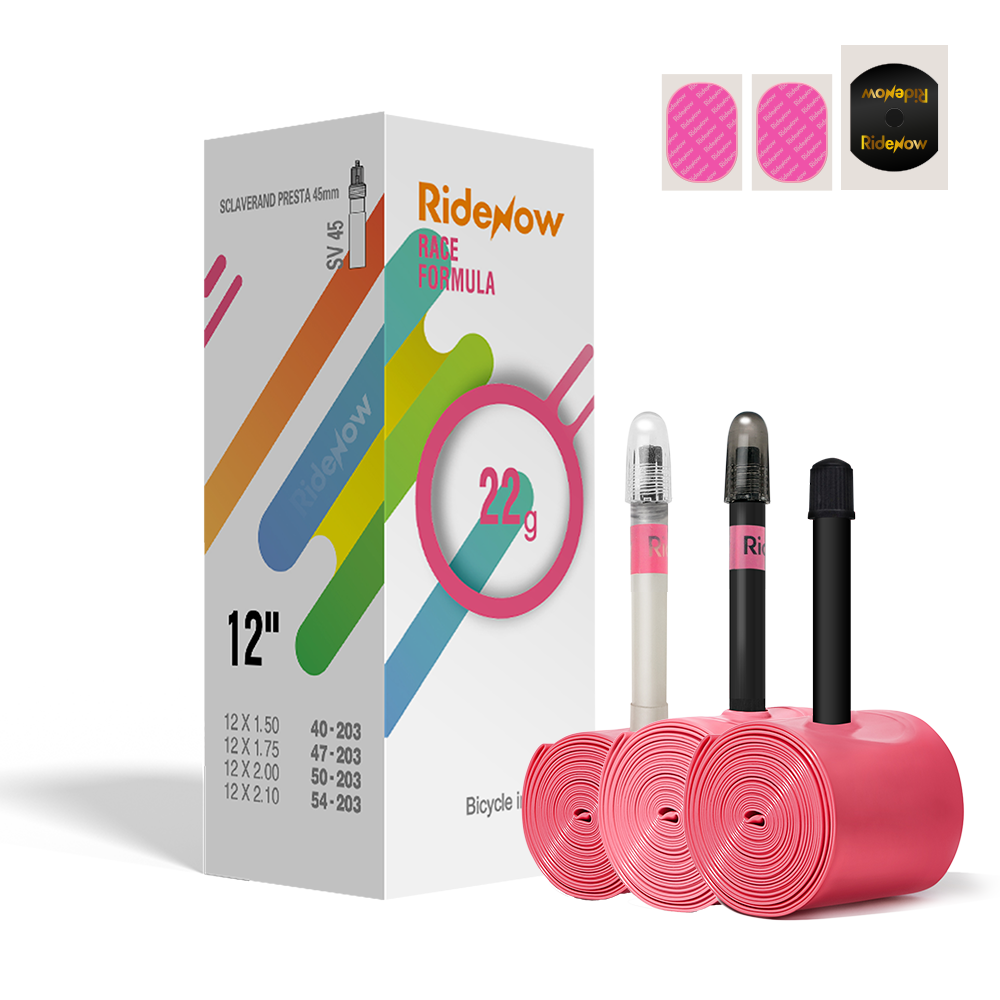
RideNow Kids Bike TPU Inner Tube 12" 203Presta/Schrader 1.3-2.0 | Ultra-light Puncture-Resistant Design Patch Kits
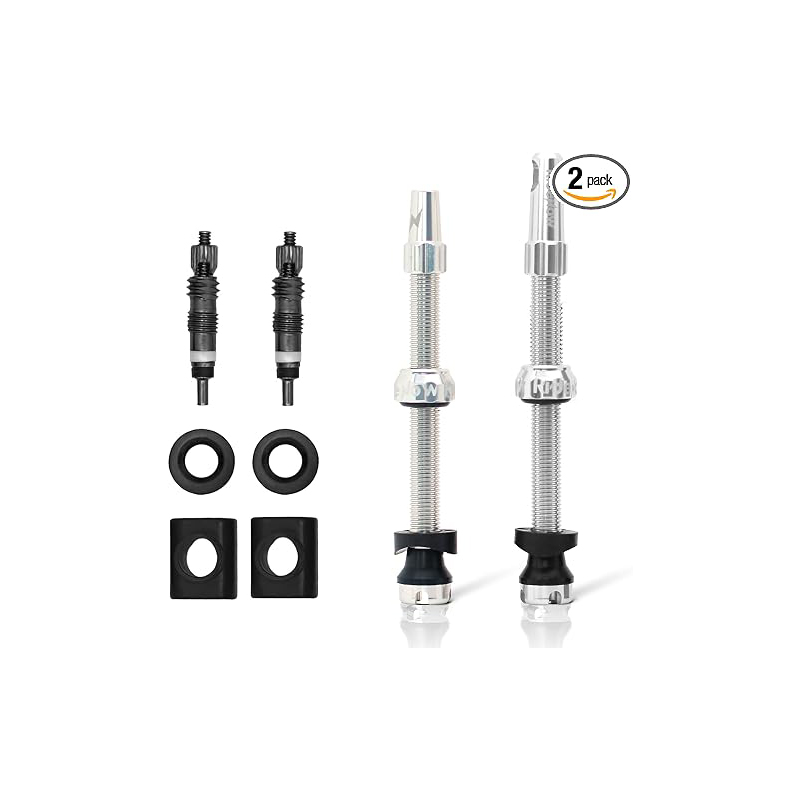
RideNow Tubeless Presta Valve Stems 7075 Aluminum Silver Pair | Ultra-light Design Removable Valve Core Remover Bicycle
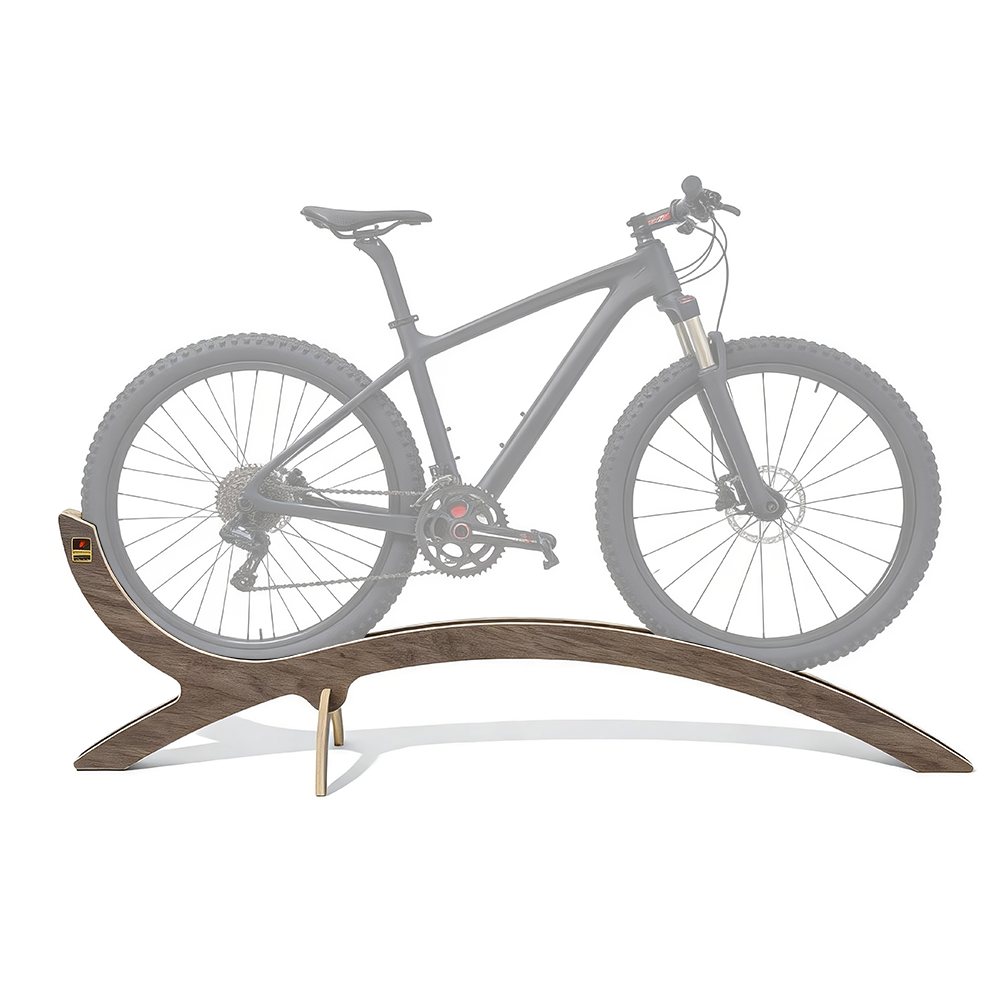
Bike Display Stand for Complete Bike Show, Strong and Easy, E0 Environmental Material, Fits MTB
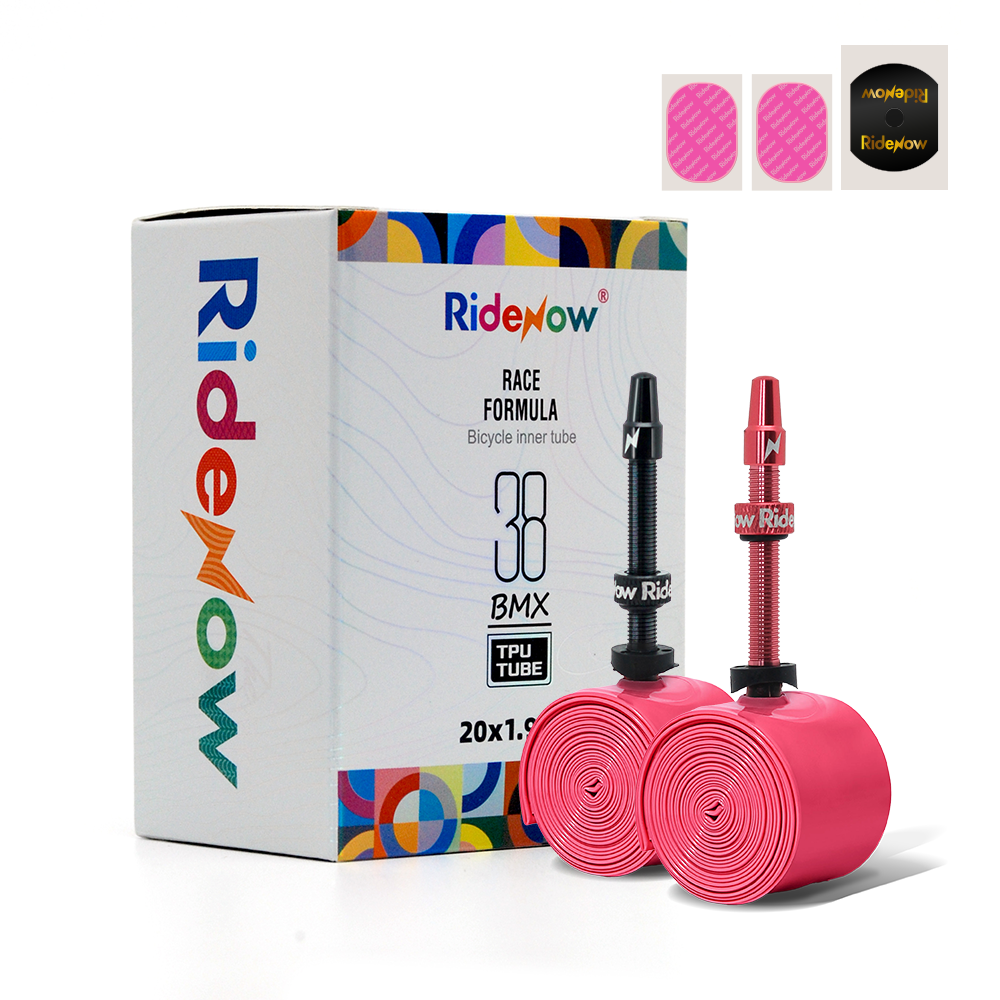
RideNow BMX Bike TPU Inner Tube 20" Presta metal vavel 45mm | Ultra-light Puncture-Resistant Design Patch Kits Included Easy
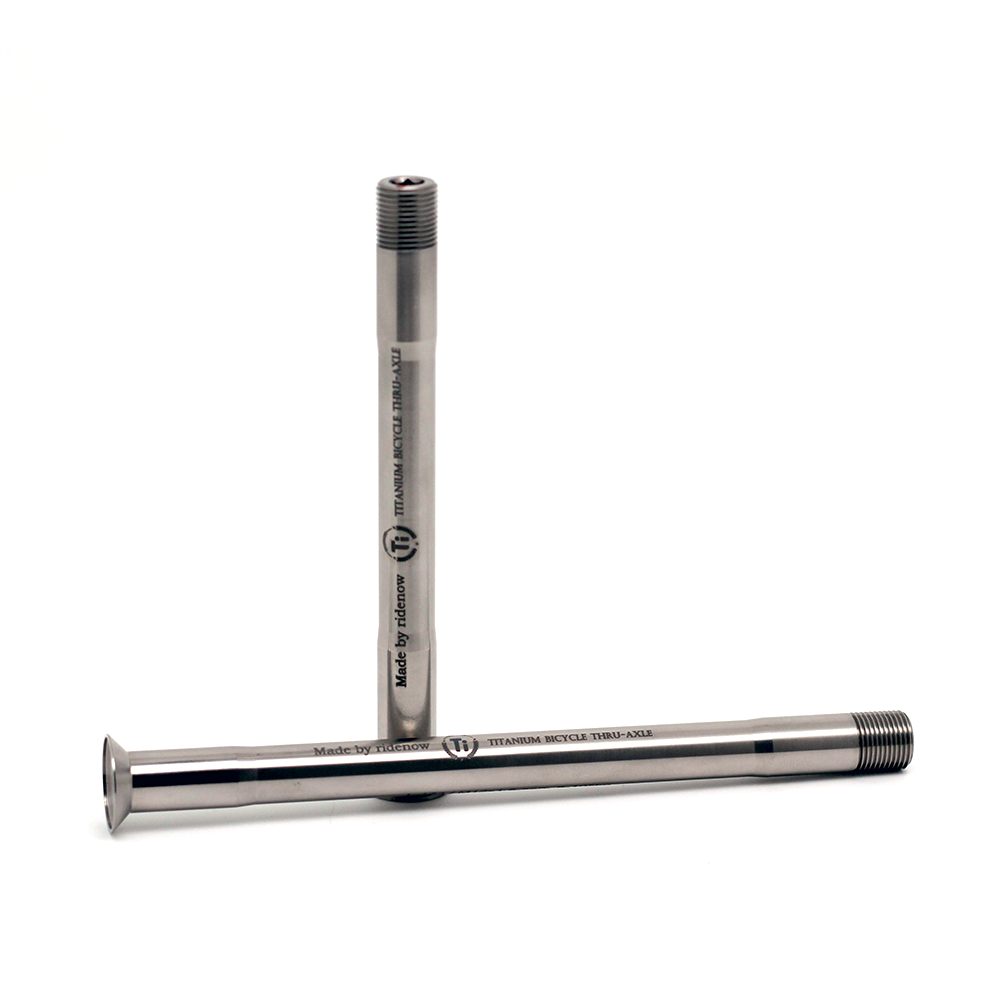
RideNow Titanium Thru-Axle Aerospace-Grade Alloy, 2x Strength of Steel, 50% Lighter, Corrosion-Resistant, Premium Wood Gift Box
Industry Whitepaper: Engineering Standards for CE Certified Cassette Lockring Tools
In modern high-performance bicycle manufacturing and professional maintenance, the cassette lockring tool serves as a critical mechanical interface. As modern bicycle drivetrains transition to high-gear-density systems—spanning 12-speed and 13-speed electronic protocols across road, gravel, mountain, and e-bikes—the torque tolerances for installation and removal have reached strict thresholds (typically 40 Nm to 50 Nm). Precision tool manufacturing is no longer merely about shaping steel; it requires advanced metallurgy, precision CNC spline broaching, and strict compliance with European safety standards under the CE Machinery Directive (2006/42/EC) and EN ISO 12100:2010 standards.
This technical whitepaper outlines the structural requirements, metallurgical benchmarks, and quality validation processes mandatory for premium OEM export tools produced by qualified Chinese manufacturing hubs.
1. Mechanical Spline Interface & Fitment Standardization
A cassette lockring tool must maintain perfect rotational symmetry to prevent rounding off the internal splines of aluminum or alloy lockrings. Premium tool factories utilize multi-axis CNC machines and automated broaching tools to ensure precise tooth profiling across three primary industry lockring profiles:
| Spline Profile Standards | Spline Count & Outer Diameter | Primary Drivetrain Compatibility | Required Metallurgical Yield Strength |
|---|---|---|---|
| Standard Shimano HG / SRAM 12-Spline | 12 Splines / ~23.5mm OD | Shimano HG (Road/MTB), SRAM PG series, Centerlock Disc Rotors | > 850 MPa (CR-V Steel 50BV30) |
| Campagnolo Ultra-Torque / Lockring | 12 Splines / ~23.0mm OD (Deeper Cut) | Campagnolo 9-13 speed cassettes, older Campagnolo bottom brackets | > 900 MPa (S2 Hardened Steel) |
| Micro Spline & SRAM XD/XDR Freehubs | 12 Splines with Guide Pin / Extended Depth | Shimano 12s Micro Spline, SRAM XD/XDR 11/12s high-torque setups | > 950 MPa (Heat-Treated Alloy Steel) |
2. Metallurgical Composition and Thermal Treatment Protocols
Tools manufactured without high-grade metallurgical control risk failure via torsional fatigue, micro-cracking, or permanent spline shearing under high torque loads. Industrial tool exporters adhere to strict material selections:
- Chrome-Vanadium Alloy Steel (Cr-V / 50BV30): The global benchmark for heavy-duty workshop tools, delivering superior toughness and high elastic limits under dynamic torque impact.
- S2 Tool Steel Grade: Preferred for ultra-slim professional mobile tools, offering higher tensile yield strength (>1200 MPa) and resistance to brittleness after hardening.
- Controlled Quenching & Tempering: Vacuum heat treatment achieves a precise Rockwell C scale hardness of HRC 48–52, striking an optimal balance between outer tooth wear resistance and inner core shock absorption.
3. CE Certification & Structural Compliance
To comply with European Market import regulations, professional cassette lockring tools manufactured by export-ready factories undergo rigorous audit procedures. CE certification guarantees:
Torsional Load Testing
Verification that tools withstand a minimum of 1.5x maximum recommended industry torque (exceeding 75 Nm) without permanent structural deformation.
Chemical Hazard Safety
Compliance with EU REACH and RoHS regulations regarding heavy metals in surface finishes (nickel plating, black oxide, or electrophoretic coatings).
Operational Ergonomics
Safety against slipping or catastrophic shearing during manual lever application, protecting mechanics from hand and wrist strain.
Future Procurement Trends in Bicycle Tools & Component Sourcing
Key shifts shaping how international importers, brand managers, and wholesale distributors will source bicycle maintenance hardware over the next decade.
1. Rise of E-Bike Specific Drivetrain Maintenance Equipment
E-bikes place up to 4x the rotational torque stress on cassette lockrings and freehub bodies due to high mid-drive motor outputs. B2B procurement is rapidly shifting toward heavy-duty lockring tools featuring integrated guide pins (5mm/12mm thru-axle compatible) to prevent tool slippage under heavy workshop wrenching.
2. Multi-Hub Supply Chain Resiliency & Cross-Border Logistics
Global buyers are avoiding single-region vulnerability. Leading manufacturers now offer multi-regional operational support—combining high-volume production in mainland China with technical R&D hubs in Europe (e.g., Düsseldorf, Germany) and logistics support in Taiwan to streamline global import clearance and DDP tariffs.
3. Private-Label Customization & Low-MOQ Sampling
Distributors are moving away from unbranded generic tools toward customized private-label tooling programs. Factories offering high-precision fiber laser etching, custom anodized finishes, localized barcode packaging, and flexible starter MOQs (from 20 units) are capturing market share.
Product Development & Metallurgical Innovation Trends
As modern bicycles evolve toward clean integration and light weight, tool engineering is adopting advanced manufacturing technologies to improve durability, torque accuracy, and mechanic safety.
Integrated 1/2-Inch Drive & 24mm Hex Dual Interfaces
Modern professional lockring sockets are engineered with dual drive options: an internal 1/2" square drive for direct attachment to calibrated workshop torque wrenches, combined with a 24mm external hex profile for adjustable spanners during field repairs. This eliminates tool slop and ensures precise torque specification compliance during cassette installs.
Hardened Thru-Axle Stabilizing Pin Integration
Standard lockring tools tend to tip out of the shallow lockring teeth when applying 40+ Nm of force. Next-generation tools integrate a spring-loaded center guide pin (compatible with 12mm road/gravel and 15mm MTB thru-axles) that anchors the tool perfectly parallel inside the hub axle cavity during rotation, virtually eliminating slippage and damaged lockring teeth.
Surface Treatments: Electrophoretic Black Oxide & Manganese Phosphate
Conventional chrome plating can chip under severe torque, exposing underlying steel to oxidation. Factory innovations now favor manganese phosphate micro-coatings and advanced electrophoretic deposition (ED), offering 5x higher salt-spray corrosion resistance while preserving tight broaching tolerances.
Lightweight Hybrid CNC Aluminum-Steel Composites
For racing mechanics and travel kits, engineers are combining high-grade 7075-T6 aluminum bodies with press-fit S2 hardened steel spline rings. This hybrid construction cuts overall tool weight by over 55% while retaining full steel-to-steel contact strength where torque engagement happens.
Enterprise Infrastructure & Global Manufacturing Advantages
Backed by Qingdao JORV Technology Co., Ltd., our engineering-first culture delivers certified product quality, rapid prototyping, and flexible OEM partnerships globally.
Engineering-Driven R&D Ecosystem
Founded in 2017 by passionate cycling engineers, our technical department operates a specialized R&D center in Düsseldorf, Germany, a development hub in Shenyang, and supply-chain operations in Taiwan—ensuring product designs match European market standards.
30%+ Profit Reinvestment in R&D
We continuously reinvest over 30% of annual profits directly into testing equipment, automated CNC tooling, and material science research, expanding our portfolio to over 12 self-developed product lines across tools, inner tubes, and training gear.
Automated Quality & Rapid Fulfillment
Operating a 2,000m²+ facility with automated production lines in Qingdao, China, we guarantee strict batch-to-batch quality control, average B2B inquiry response times ≤ 13 hours, and full DDP/FOB/CIF shipping flexibility.
Frequently Asked Purchasing FAQs
Clear, authoritative answers to common questions asked by B2B importers, OEM buyers, and wholesale partners.
Request Your Custom OEM Tooling & Wholesale Quote Today
Partner with a proven CE-certified exporter. Connect with our engineering team for technical specifications, product catalog downloads, and wholesale factory pricing. Average response time within 13 hours.
Get a Quote